Production
Production of special fasteners and special bolts
Ten steps under one roof in Hagen: from bar stock to certificate.
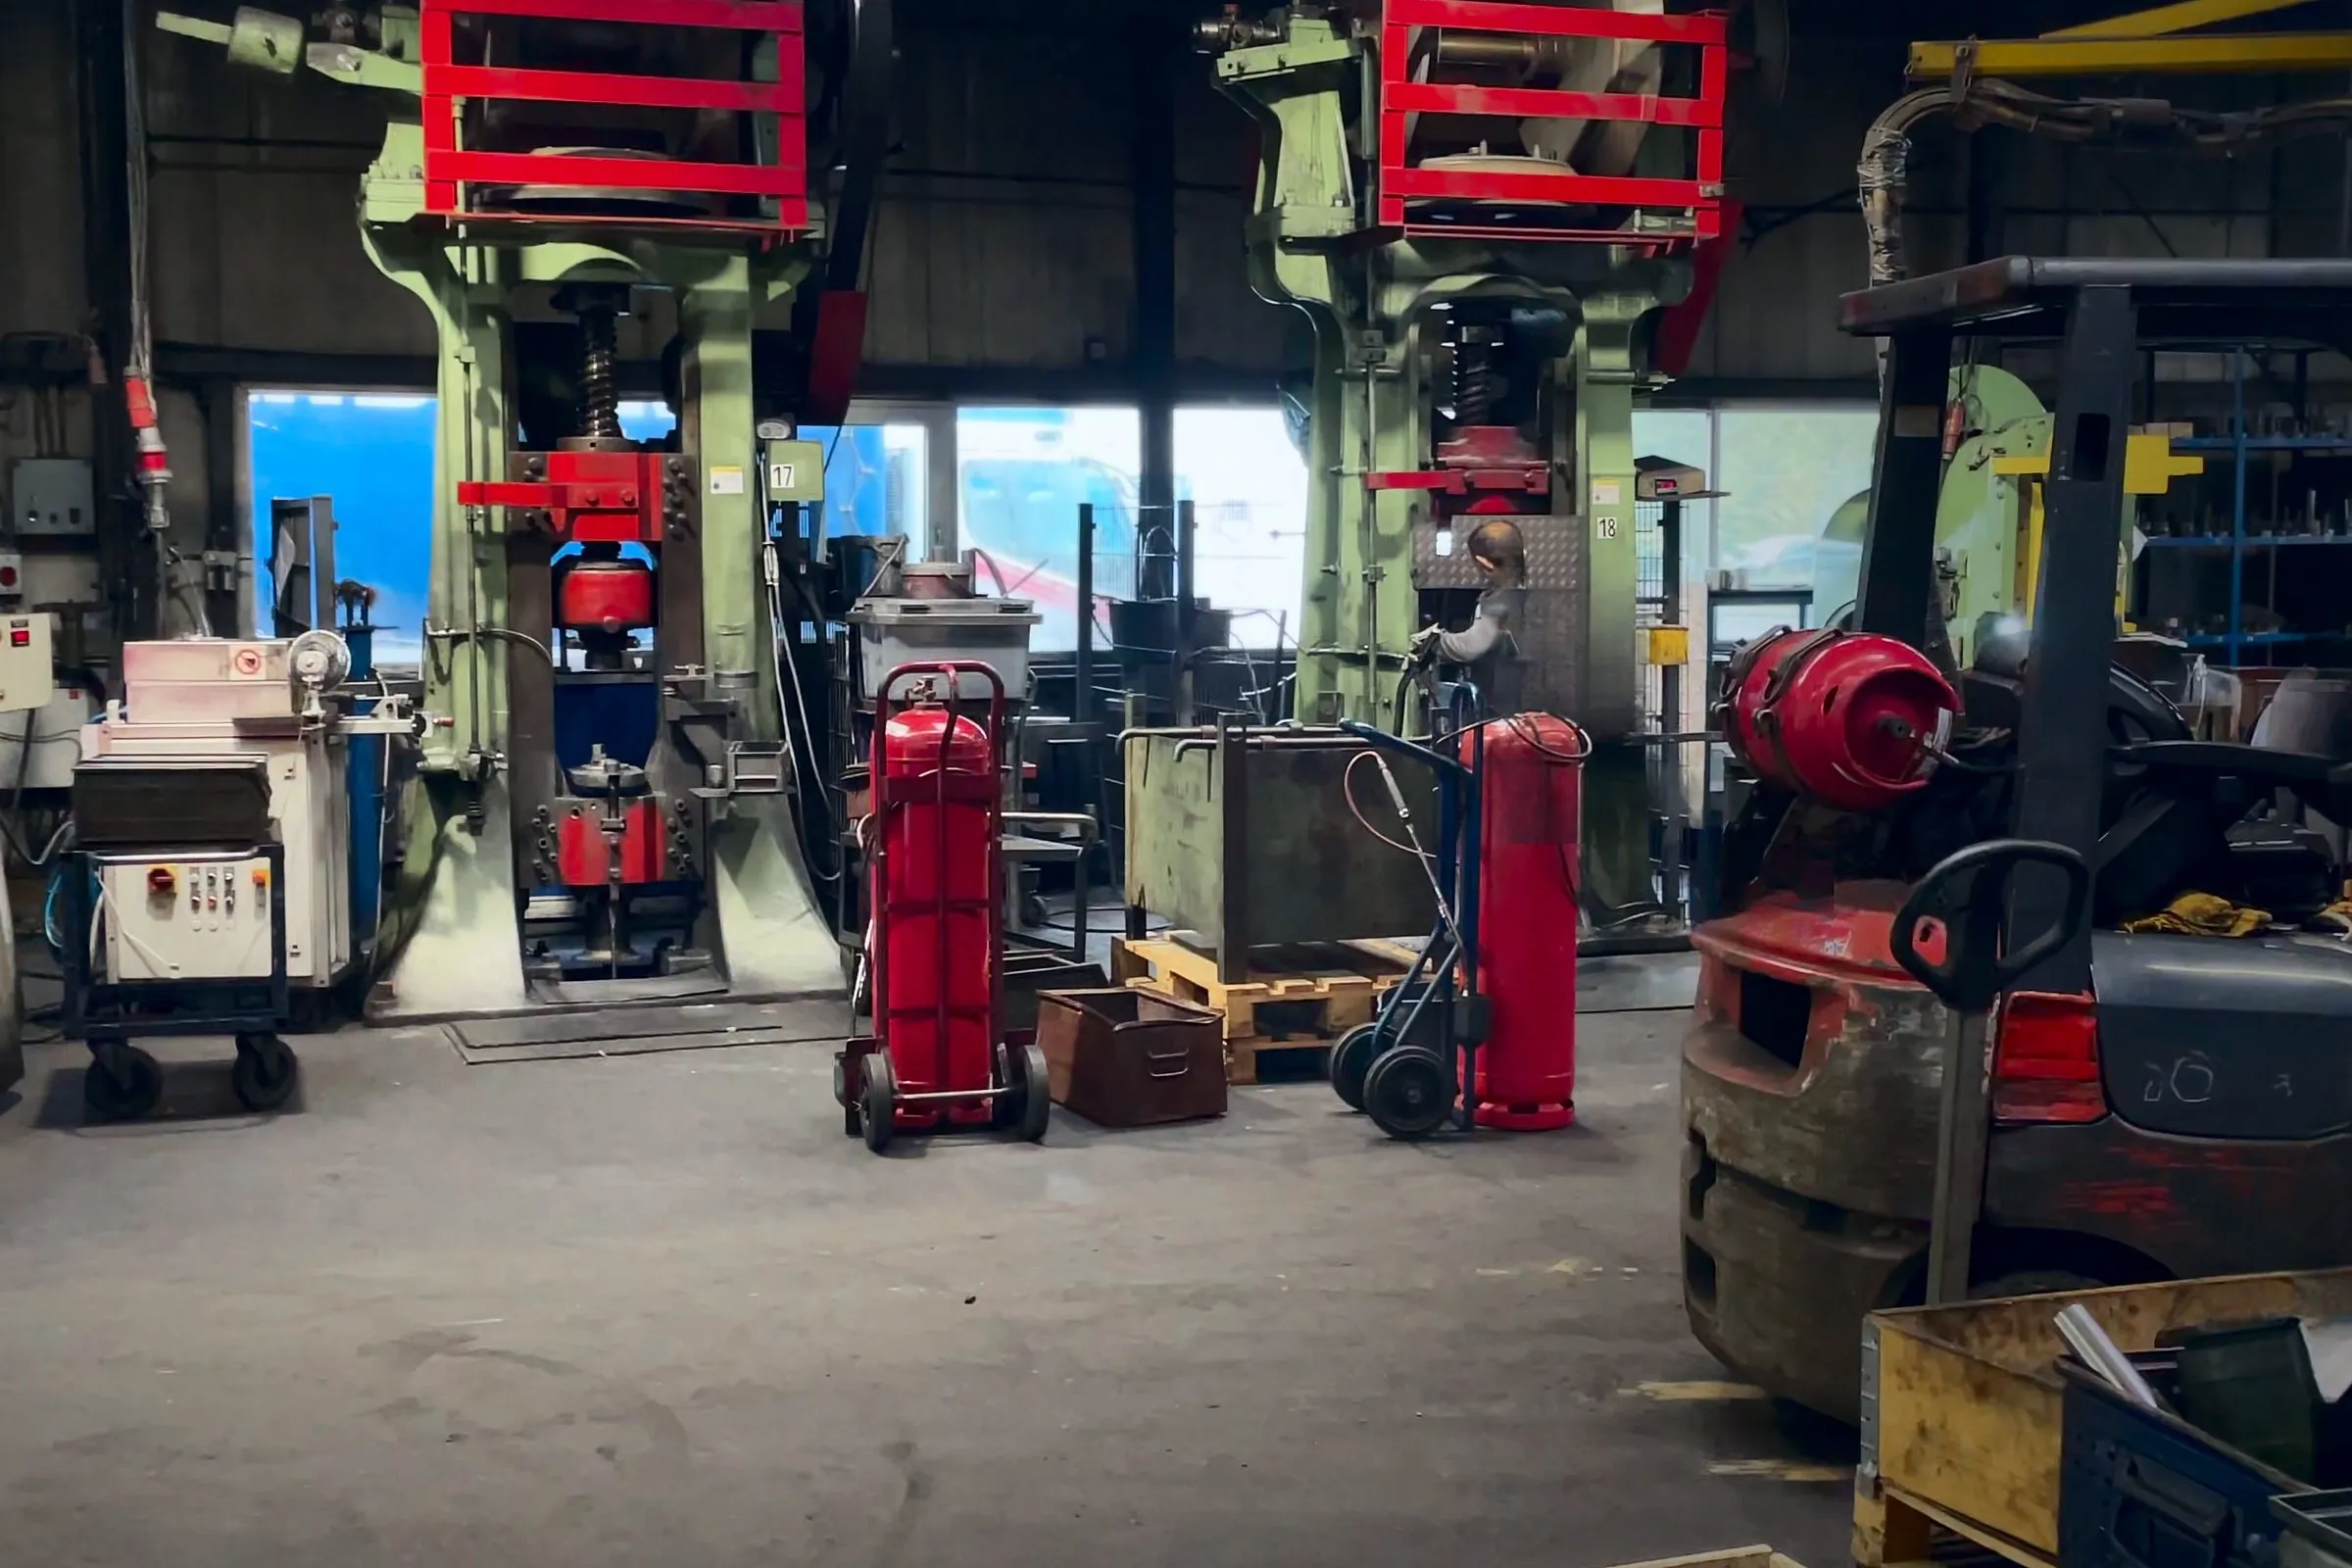
Production in Hagen
Everything from a single source: from steel to certificate
RS Randack manufactures special screws, bolts, nuts and turned parts to drawing or standard at its site in Hagen. Cutting, forging, toolmaking, machining, thread rolling, nut machining, testing and shipping are all carried out in-house. Heat treatment and coating are performed by qualified partners and verified in our own materials laboratory.
Special requirements, urgent jobs, small production runs and parts subject to third-party inspection are our daily business: parts to drawing in difficult-to-machine materials, with third-party inspection and EN 10204 3.1 or 3.2 certificates. European raw material from approved mills, production entirely in Hagen; you are welcome to visit our shop floor.
Rush orders are one of RS Randack’s strengths. You will hear from us within a few hours. In many cases, delivery within 24 hours is possible.
300 mm
Diameter of turned parts
3,500 mm
Length of turned parts
M180
Rolled threads
M80
Internal threads
3,000 kN
Tensile test
−70 °C
In-house Charpy impact test
Typical limits in each case; beyond these on request.
Ten steps
From bar stock to tested bolt
01
Cutting
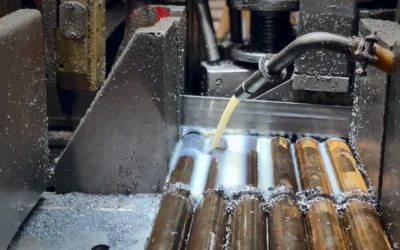
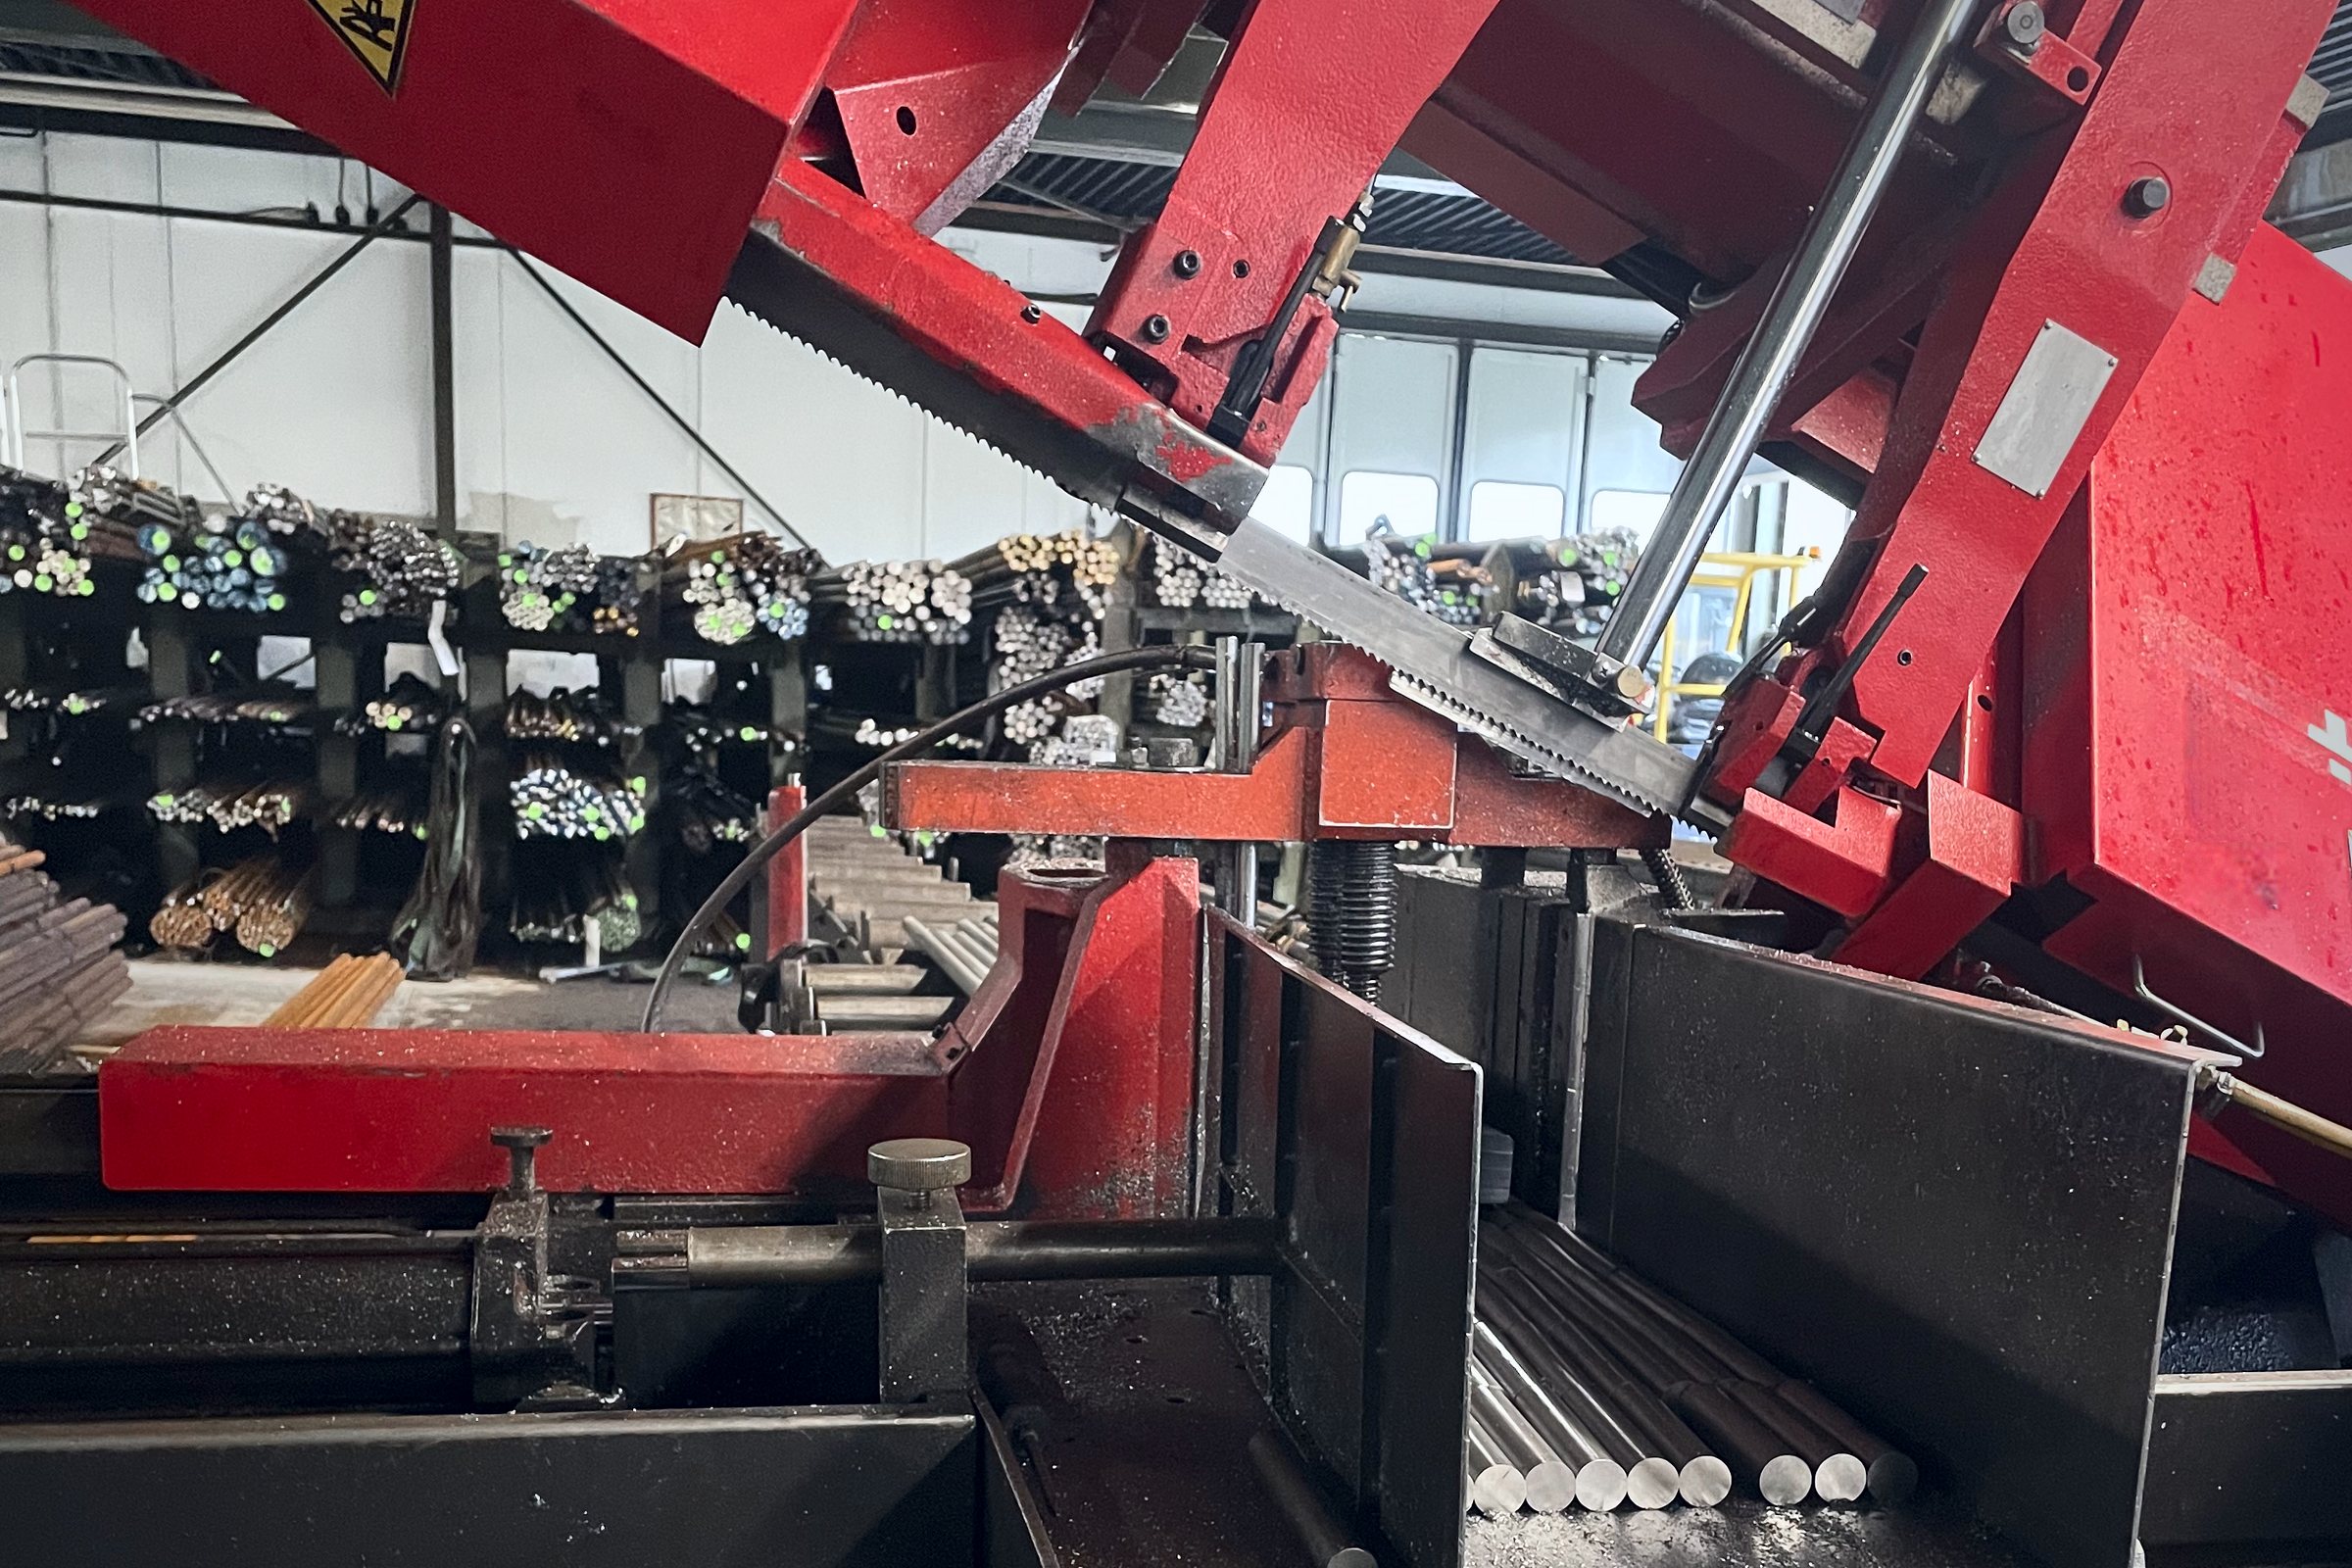
Every order starts with bar stock of verified origin. At goods receipt, dimensions, heat and batch are checked against the documents, every bar is marked, and quenched and tempered material is also tested for hardness. Five automatic band saws cut round bar up to 400 mm in diameter. Austenitic steels are processed separately. The batch remains traceable right through to the certificate.
02
Forging
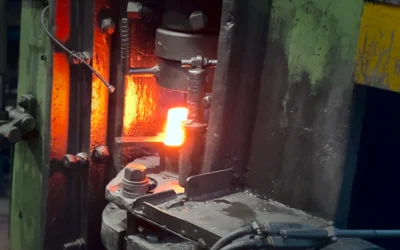
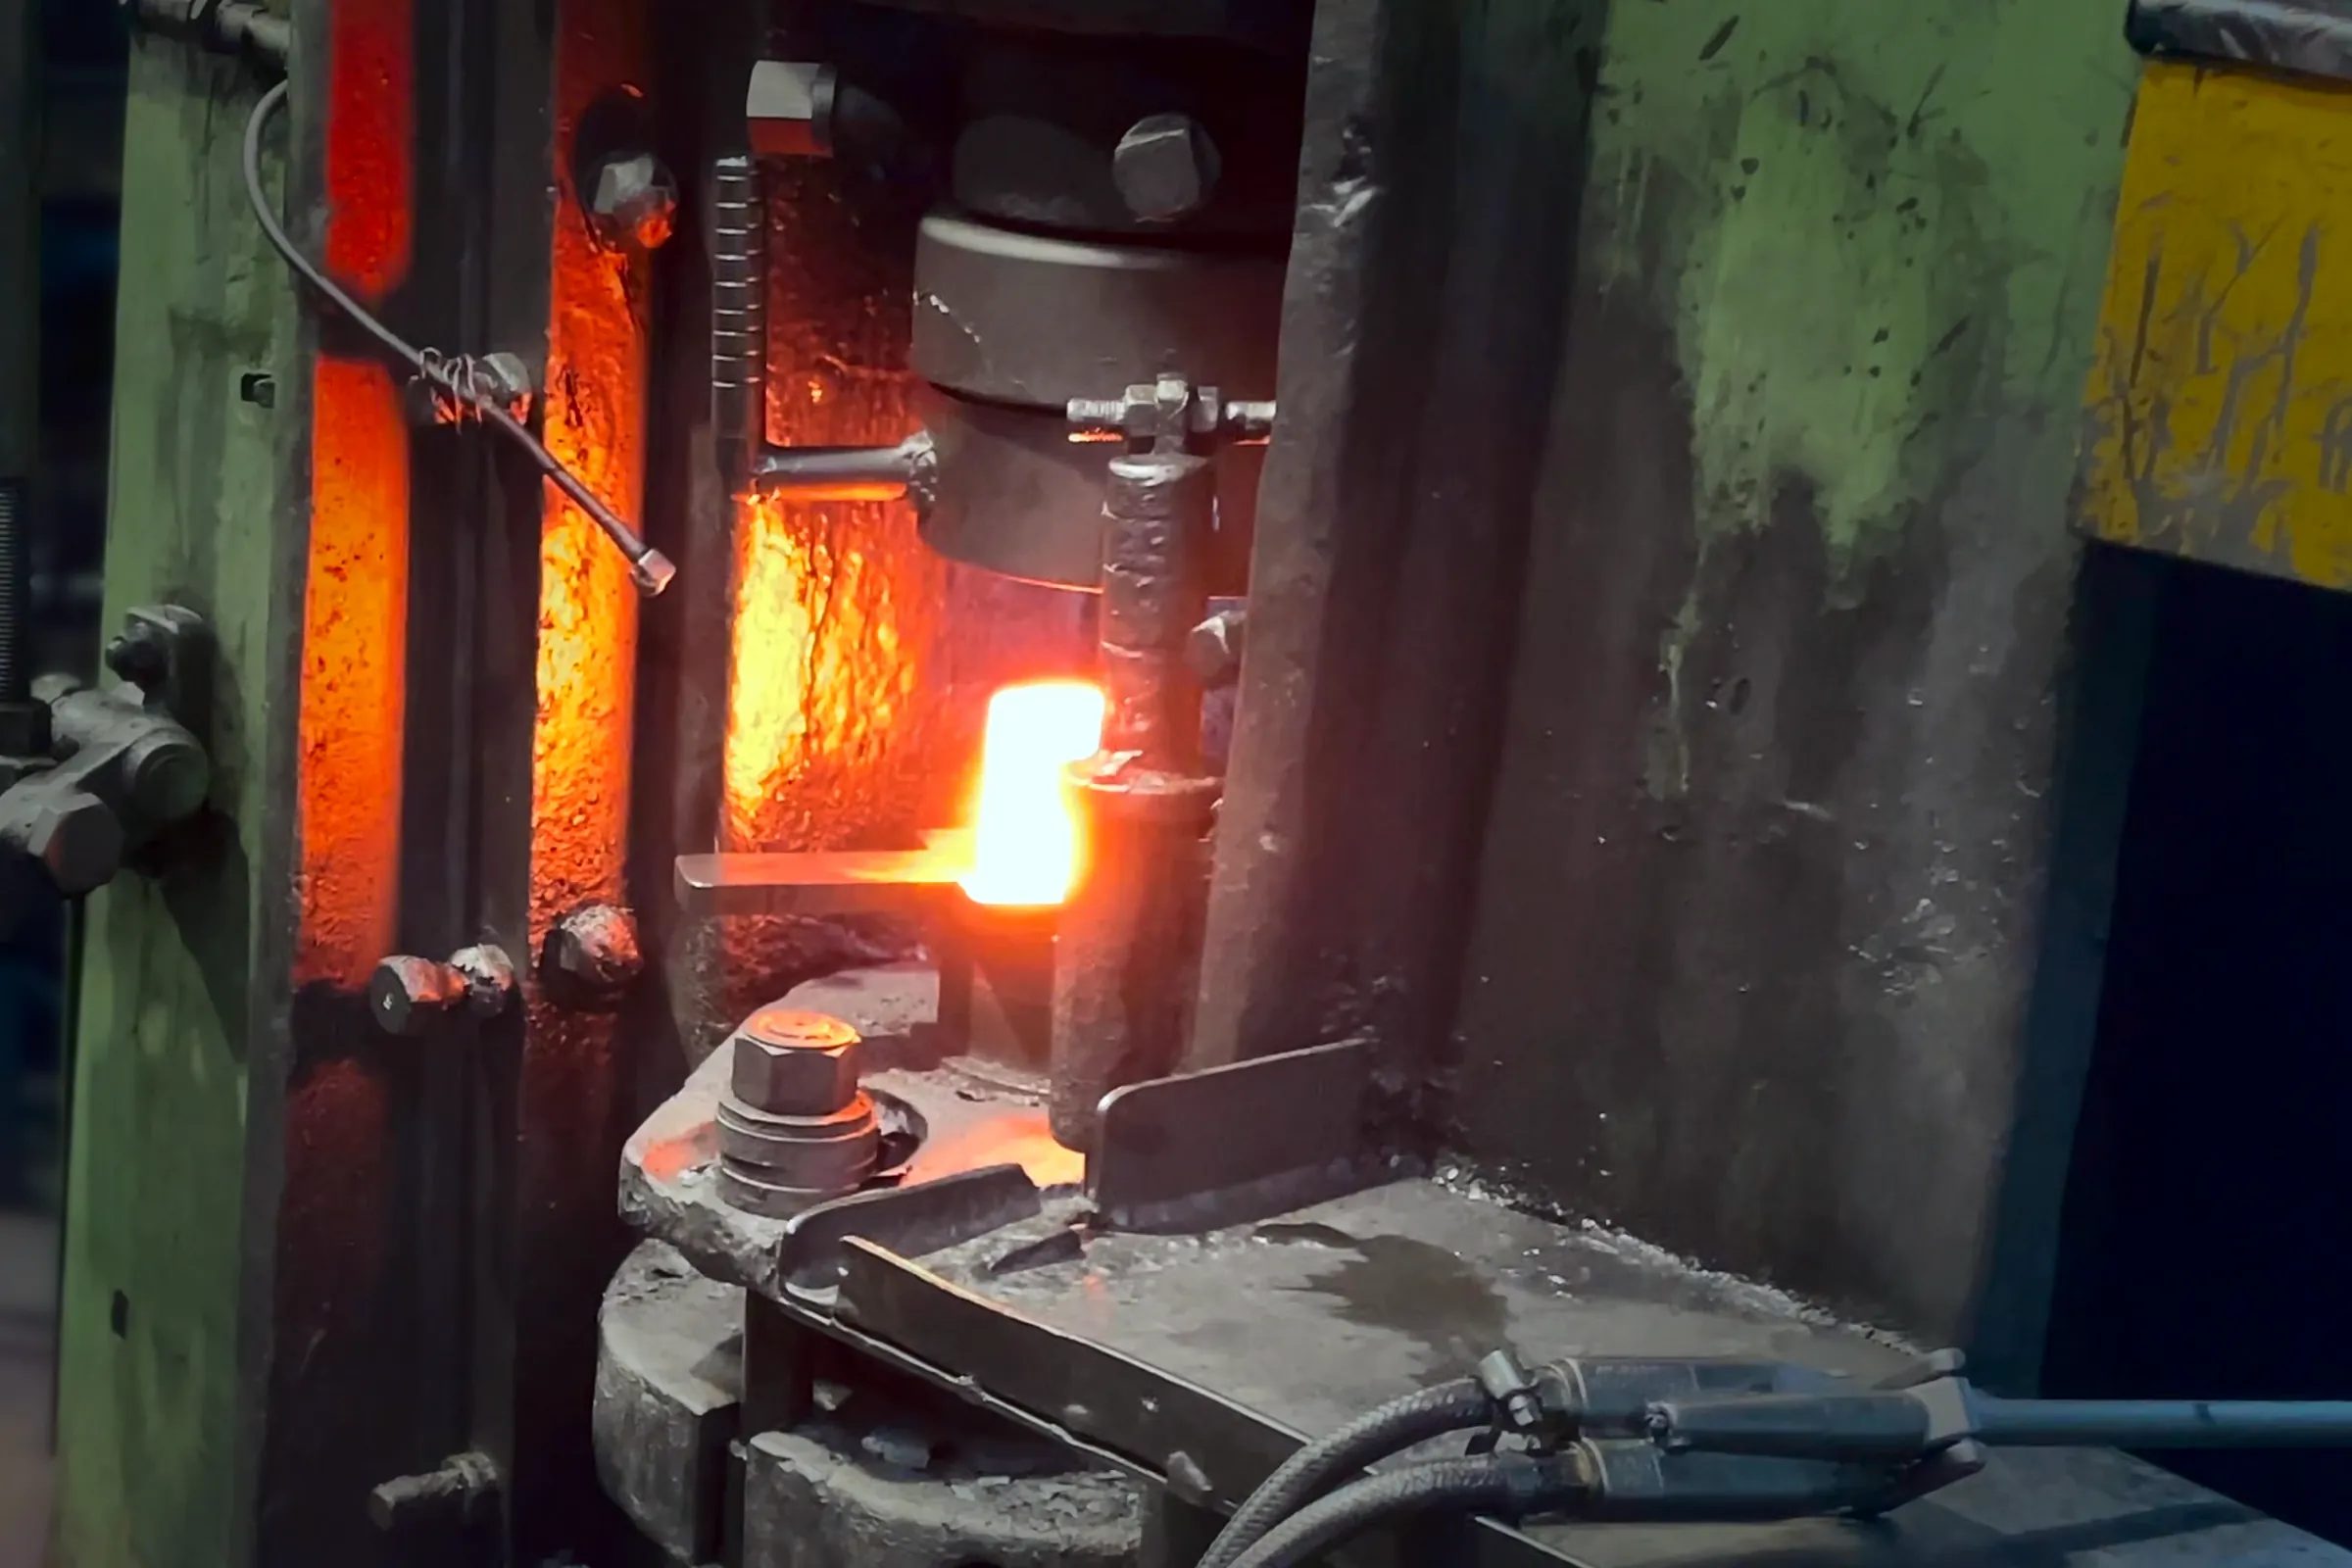
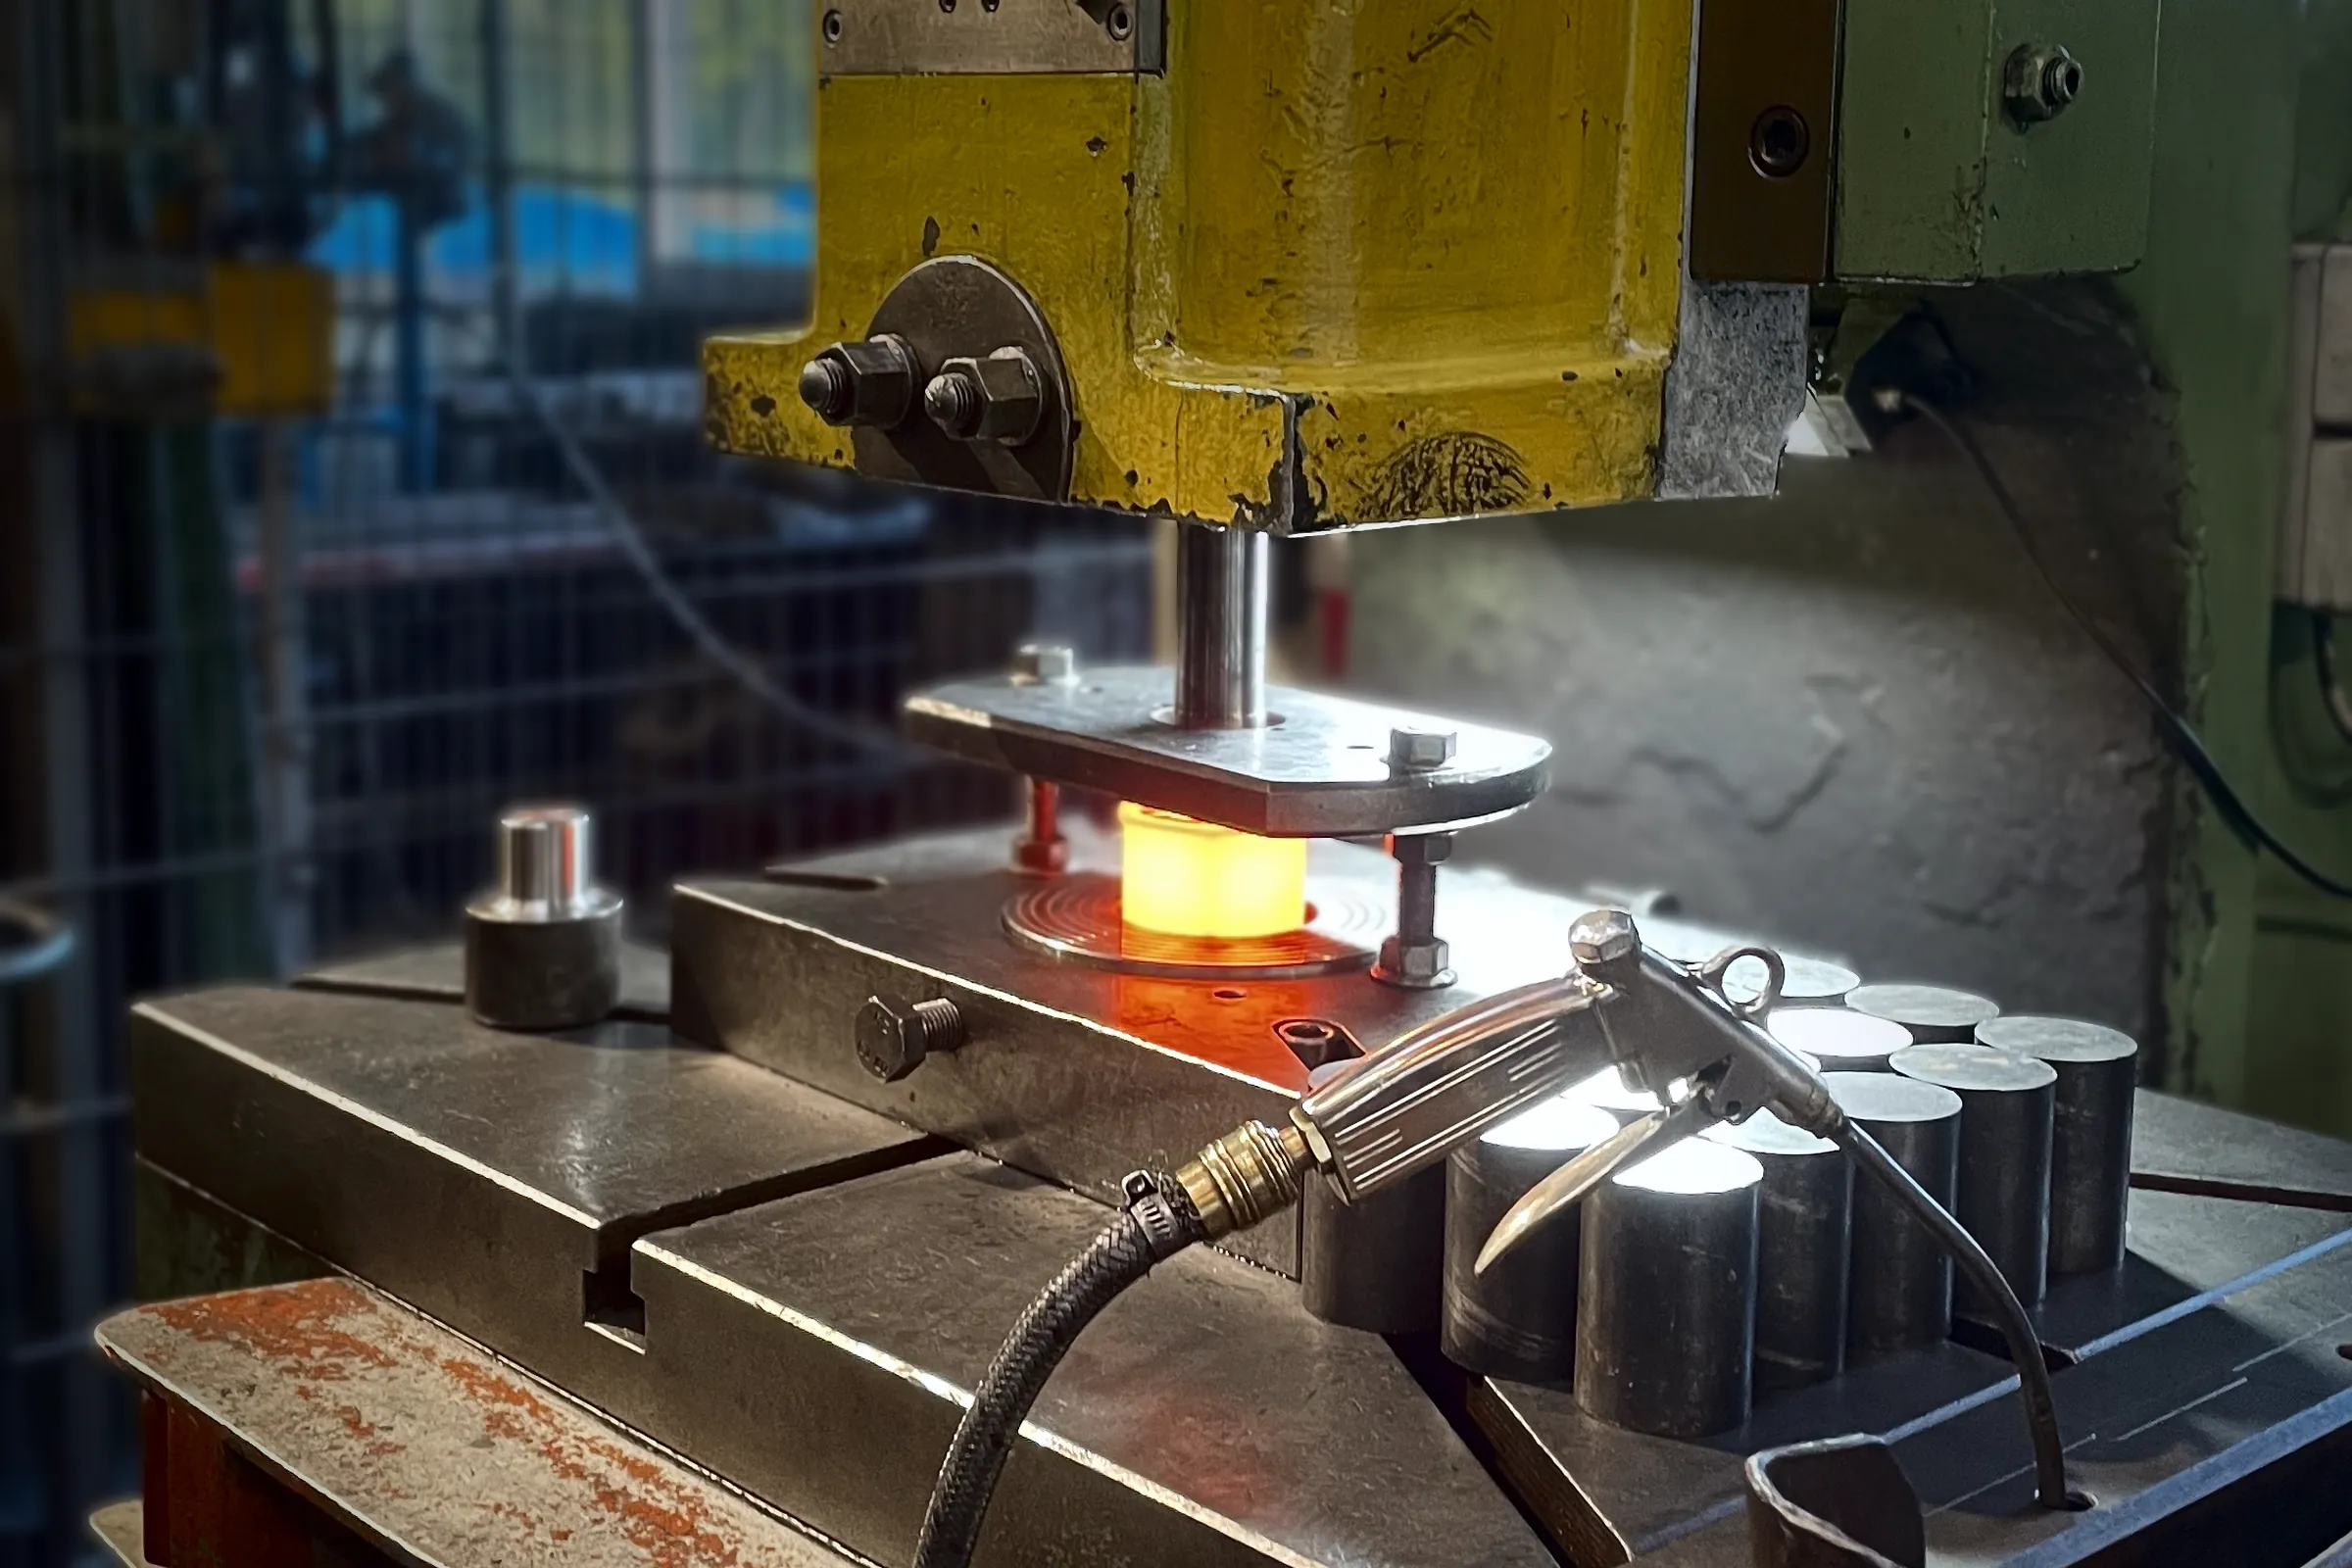
Heads, collars and nut blanks are hot-formed in our own forge, not bought in. The billets are induction-heated and die-forged on forging presses, typically up to M64, larger sizes on request. The continuous grain flow gives the head and the head-to-shank transition a strength that machined parts cannot achieve. Nuts are pierced instead of drilled.
03
Toolmaking and contract EDM
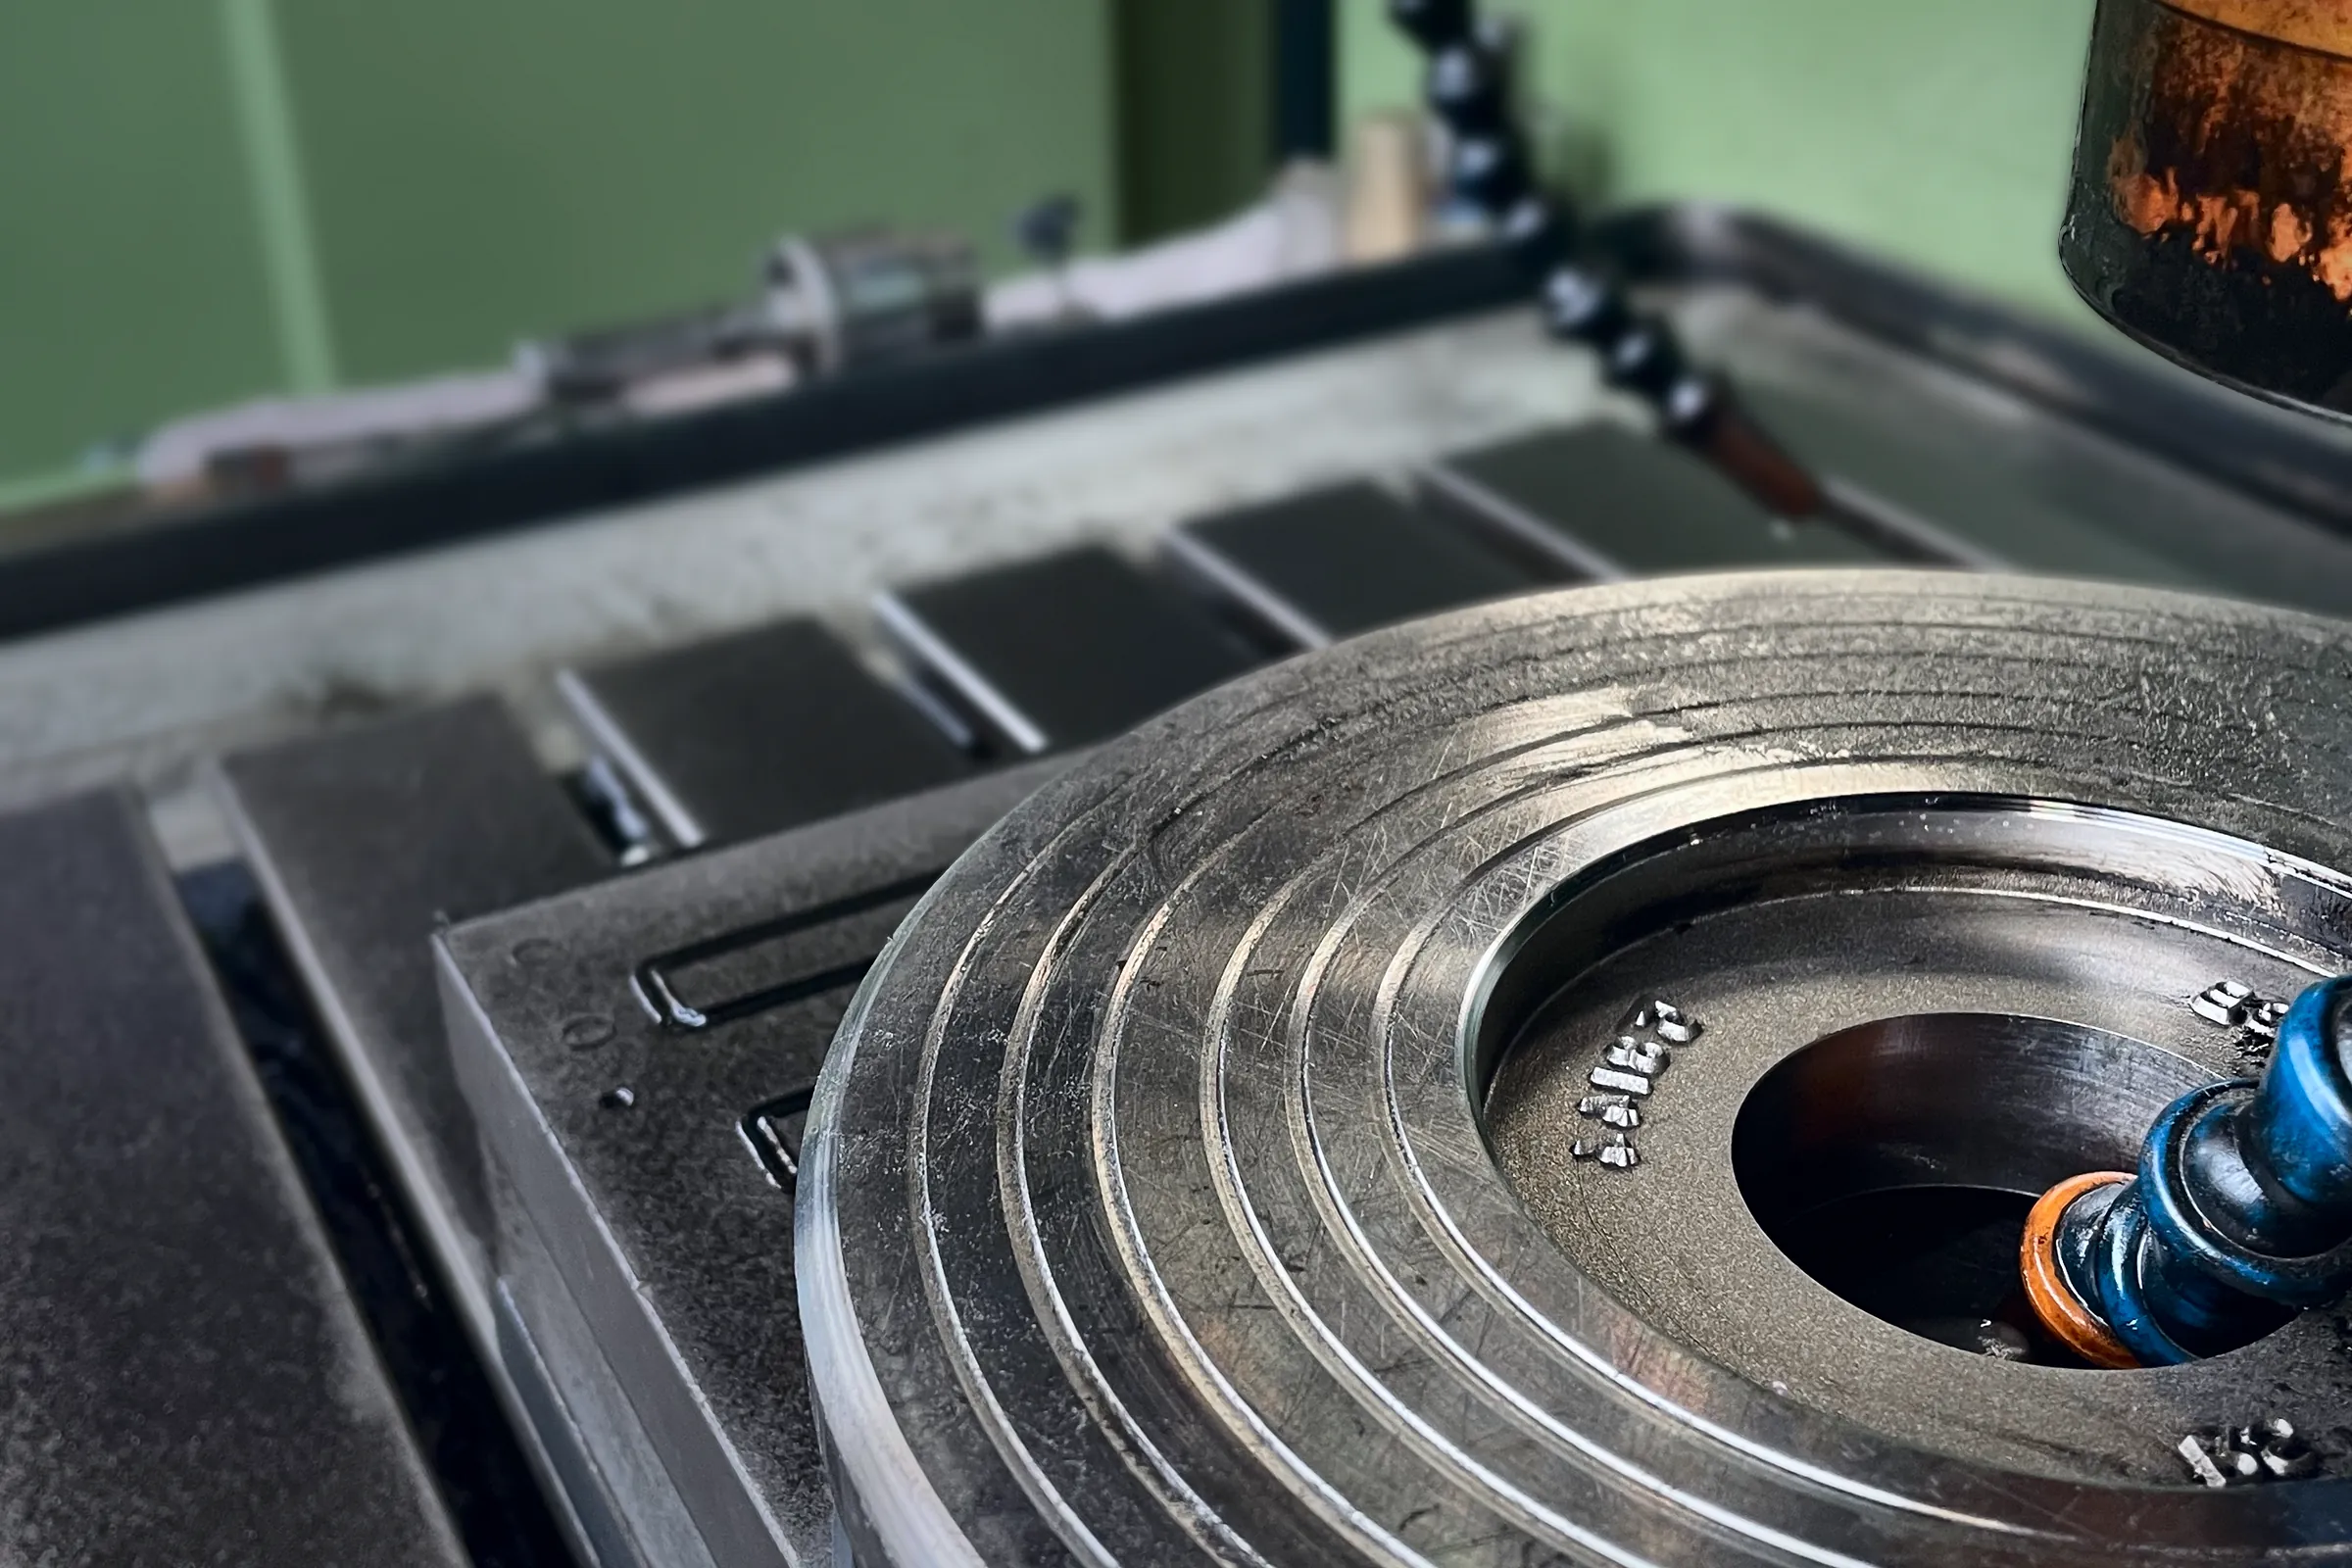
RS Randack builds dies, punches and workholding in its own toolroom, with three die-sinking EDM machines and in-house electrode manufacture. A new head shape therefore depends not on a toolmaker’s lead time but on our own machines. Spare capacity is also available for contract EDM: just call or email us.
04
Heat treatment
Quenching and tempering and other heat treatments are carried out by qualified partners with whom RS Randack has worked closely for many years. This step determines the property class. It is verified in our own materials laboratory: hardness testing per batch, tensile test on the companion test bar, microstructural examination on a micrograph. The lot moves on only once it has passed.
05
CNC machining
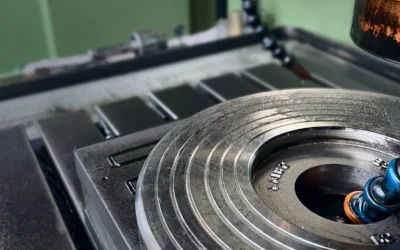
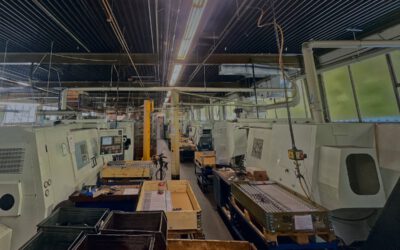
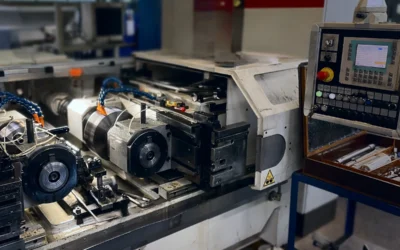
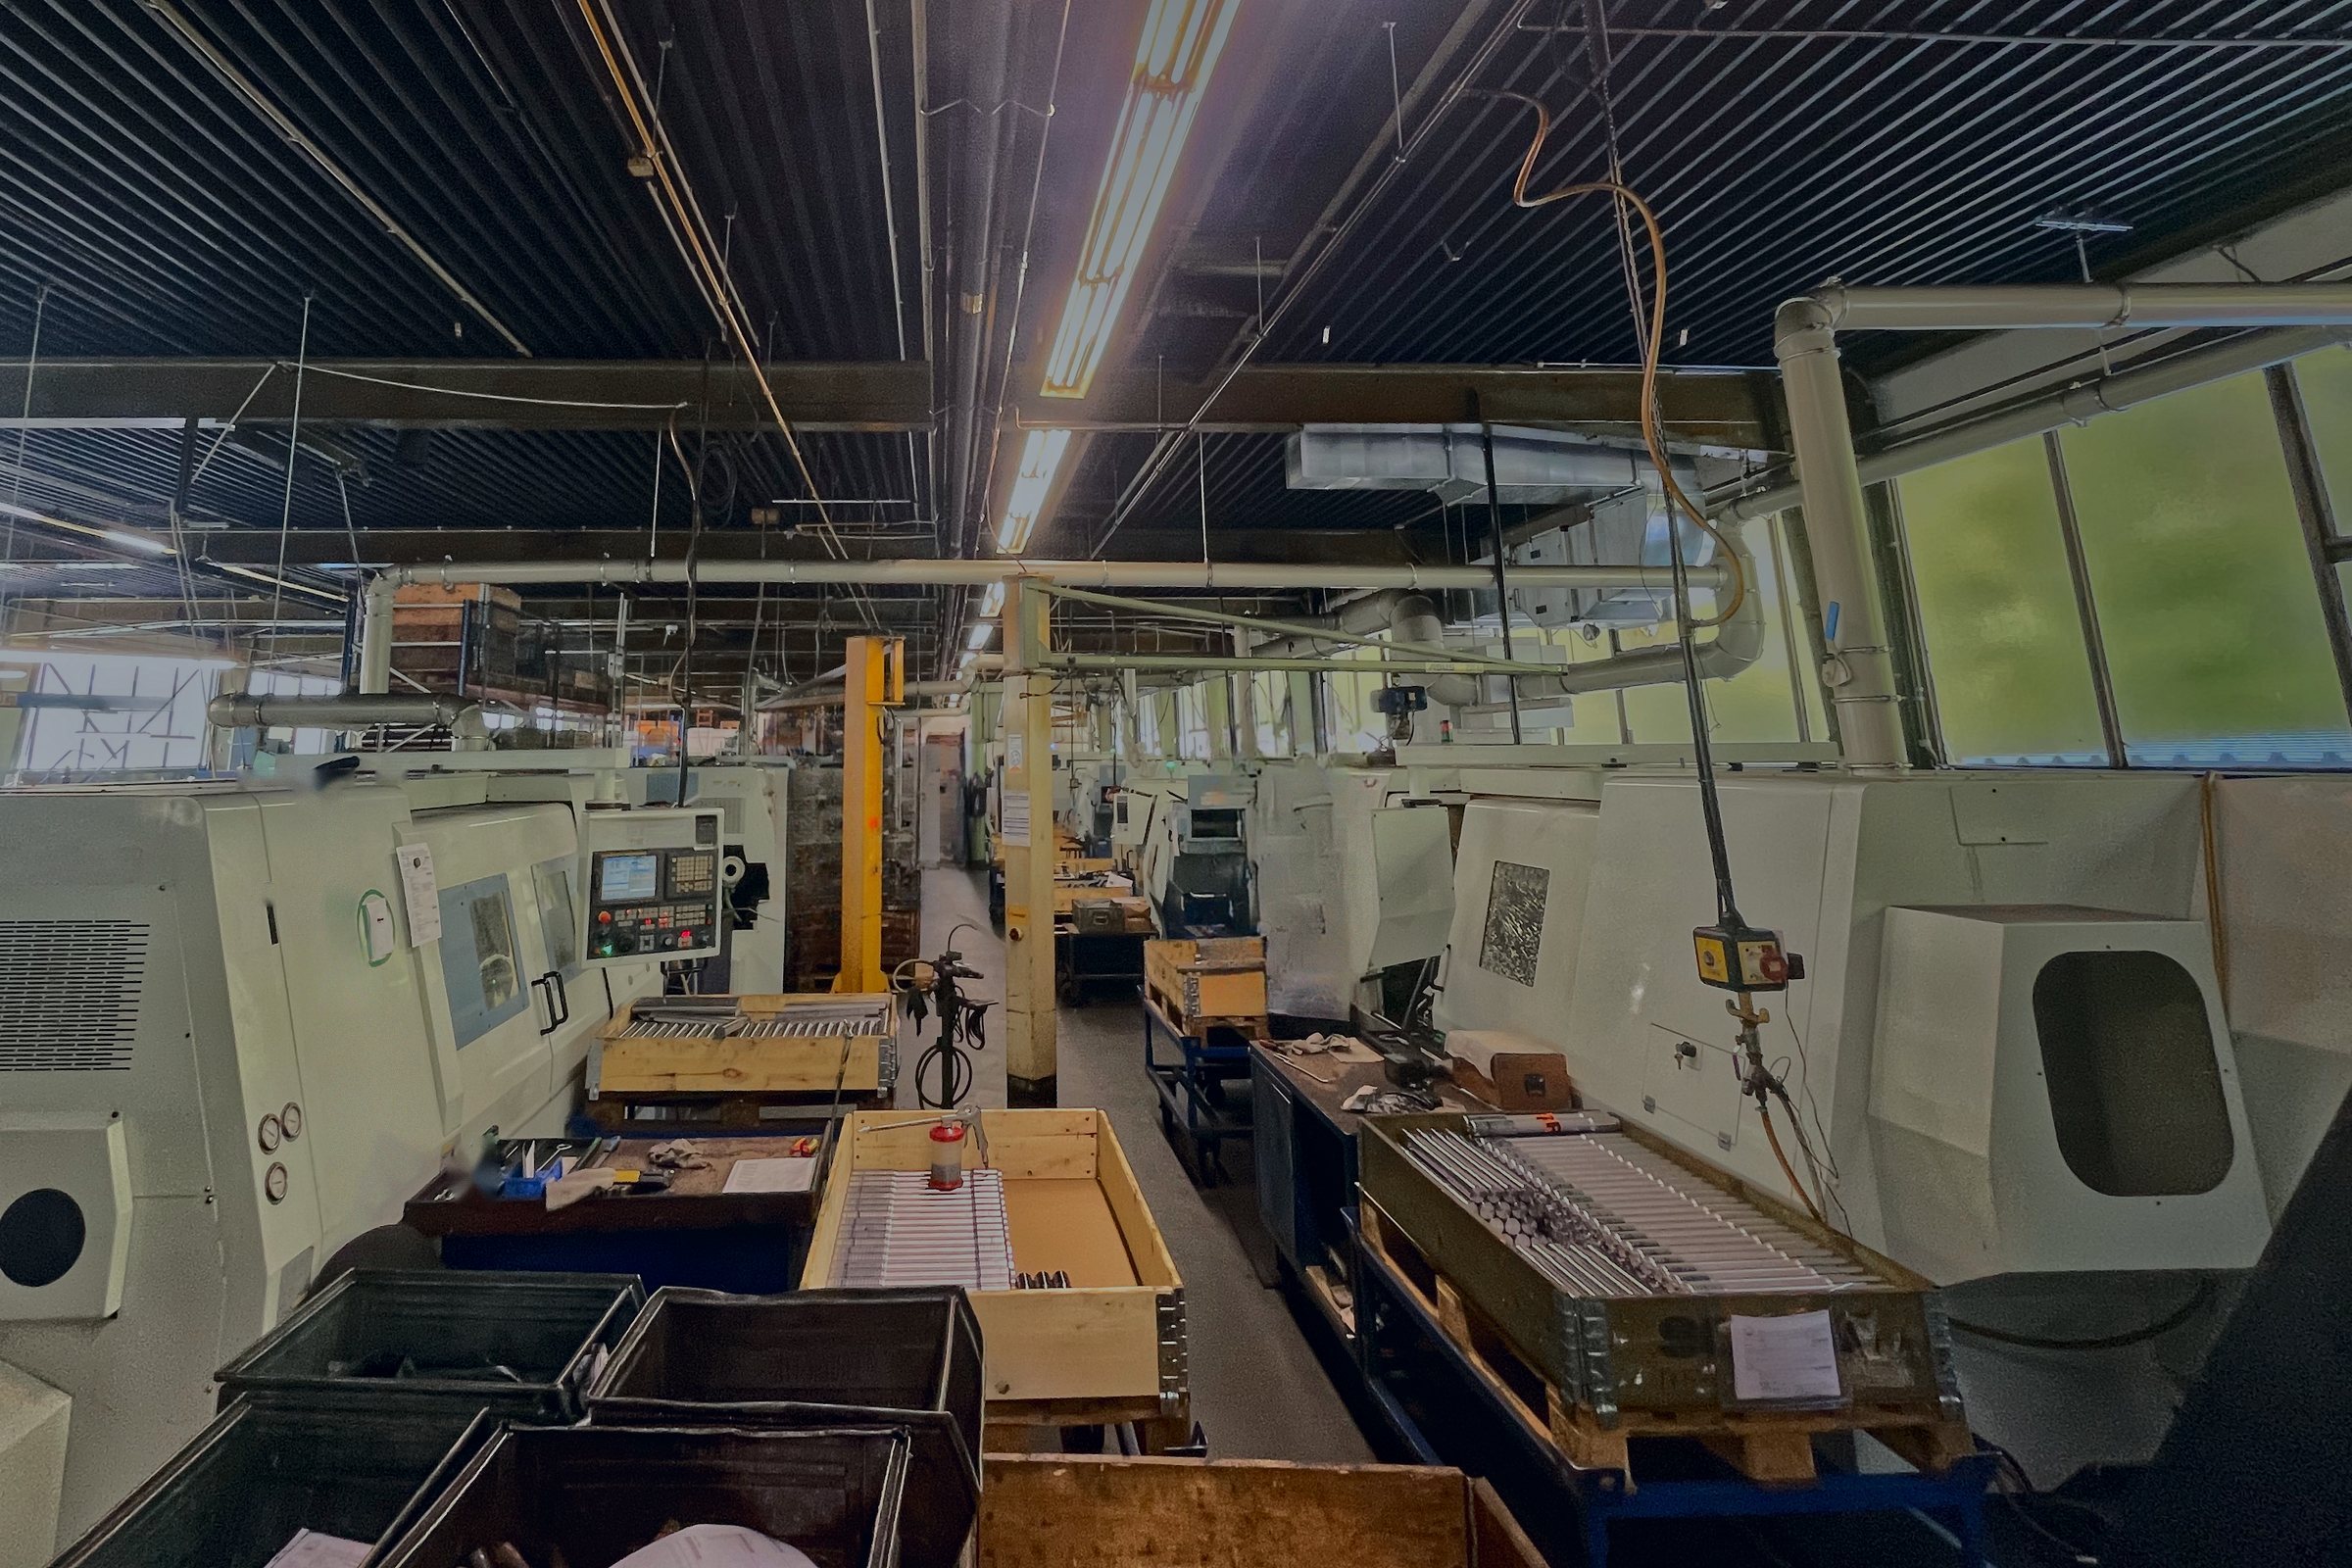
CNC turning centres produce screws, bolts and turned parts typically up to 300 mm in diameter and 3,500 mm in length, larger on request. Long, slender parts are supported with a steady rest, and difficult-to-machine materials such as duplex or high-temperature alloys are part of everyday work. Programming, workholding and maintenance are handled in-house; every lot starts with a documented first article inspection under the four-eyes principle.
06
Thread rolling
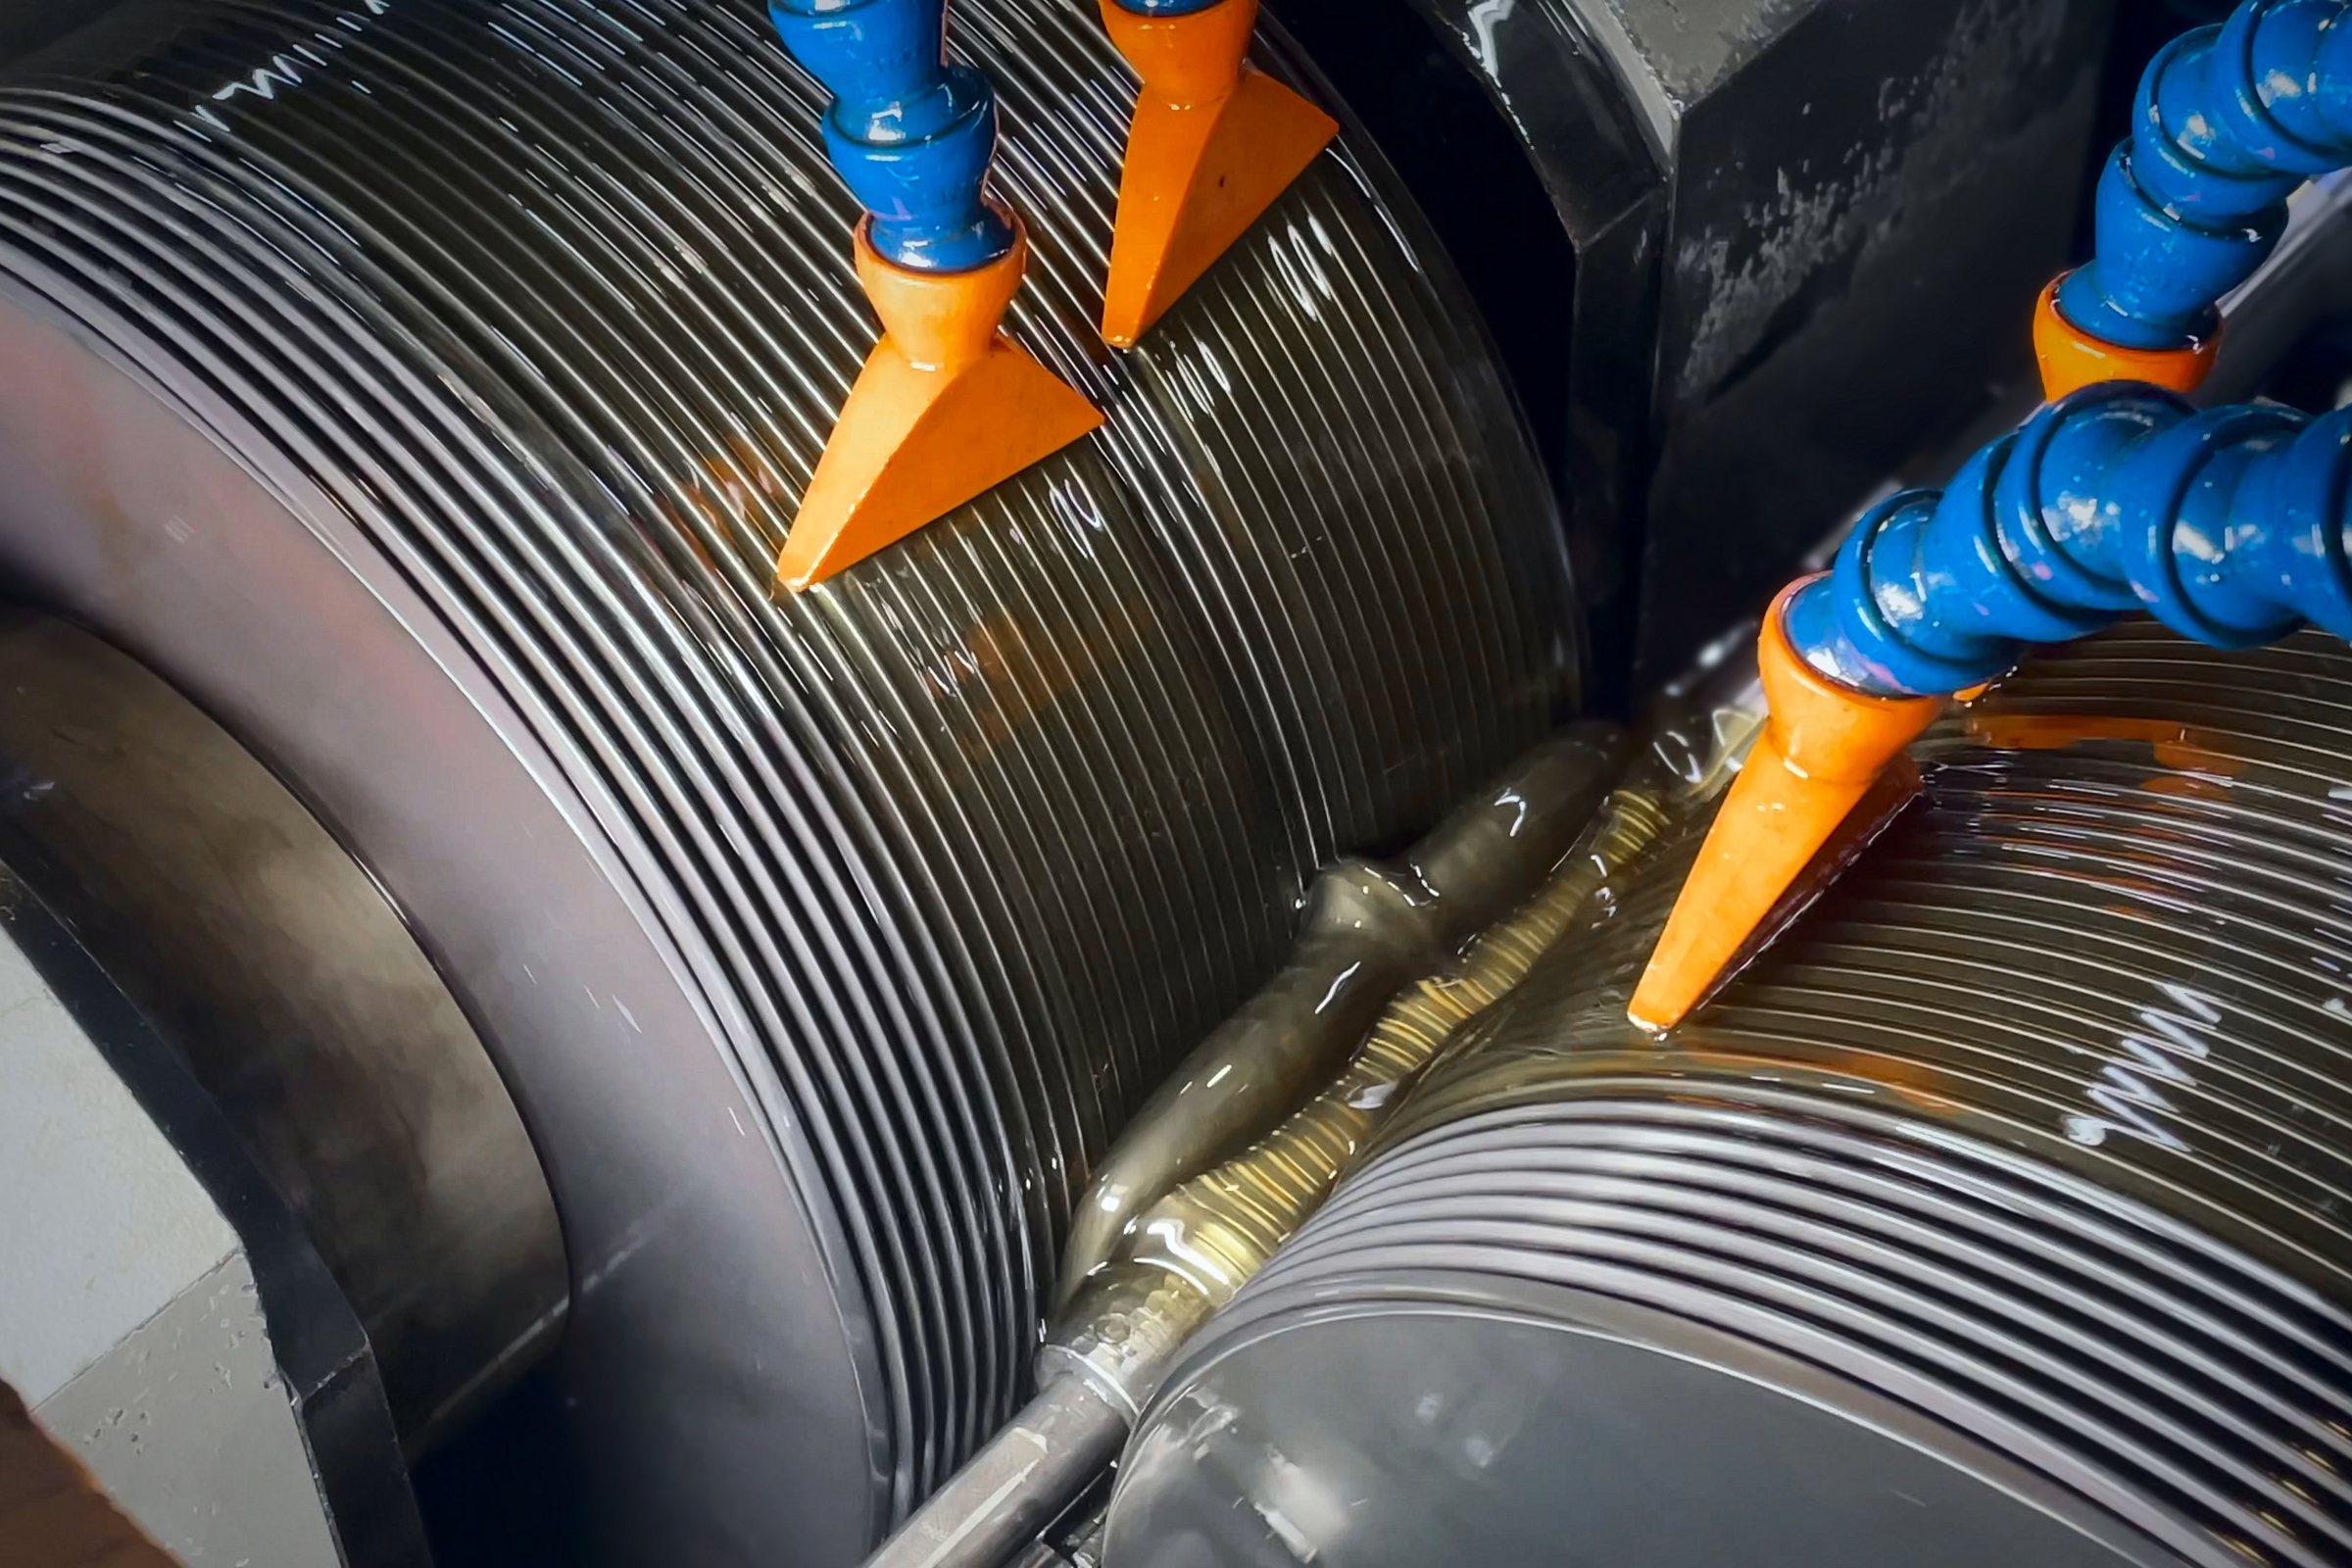
By far the majority of all threads at RS Randack are rolled, not cut: cold-formed with continuous grain flow and a compacted surface, and on request rolled after quenching and tempering. Threads typically up to M180, larger on request; metric, inch and American profiles such as UN and UNR.
07
Nut machining
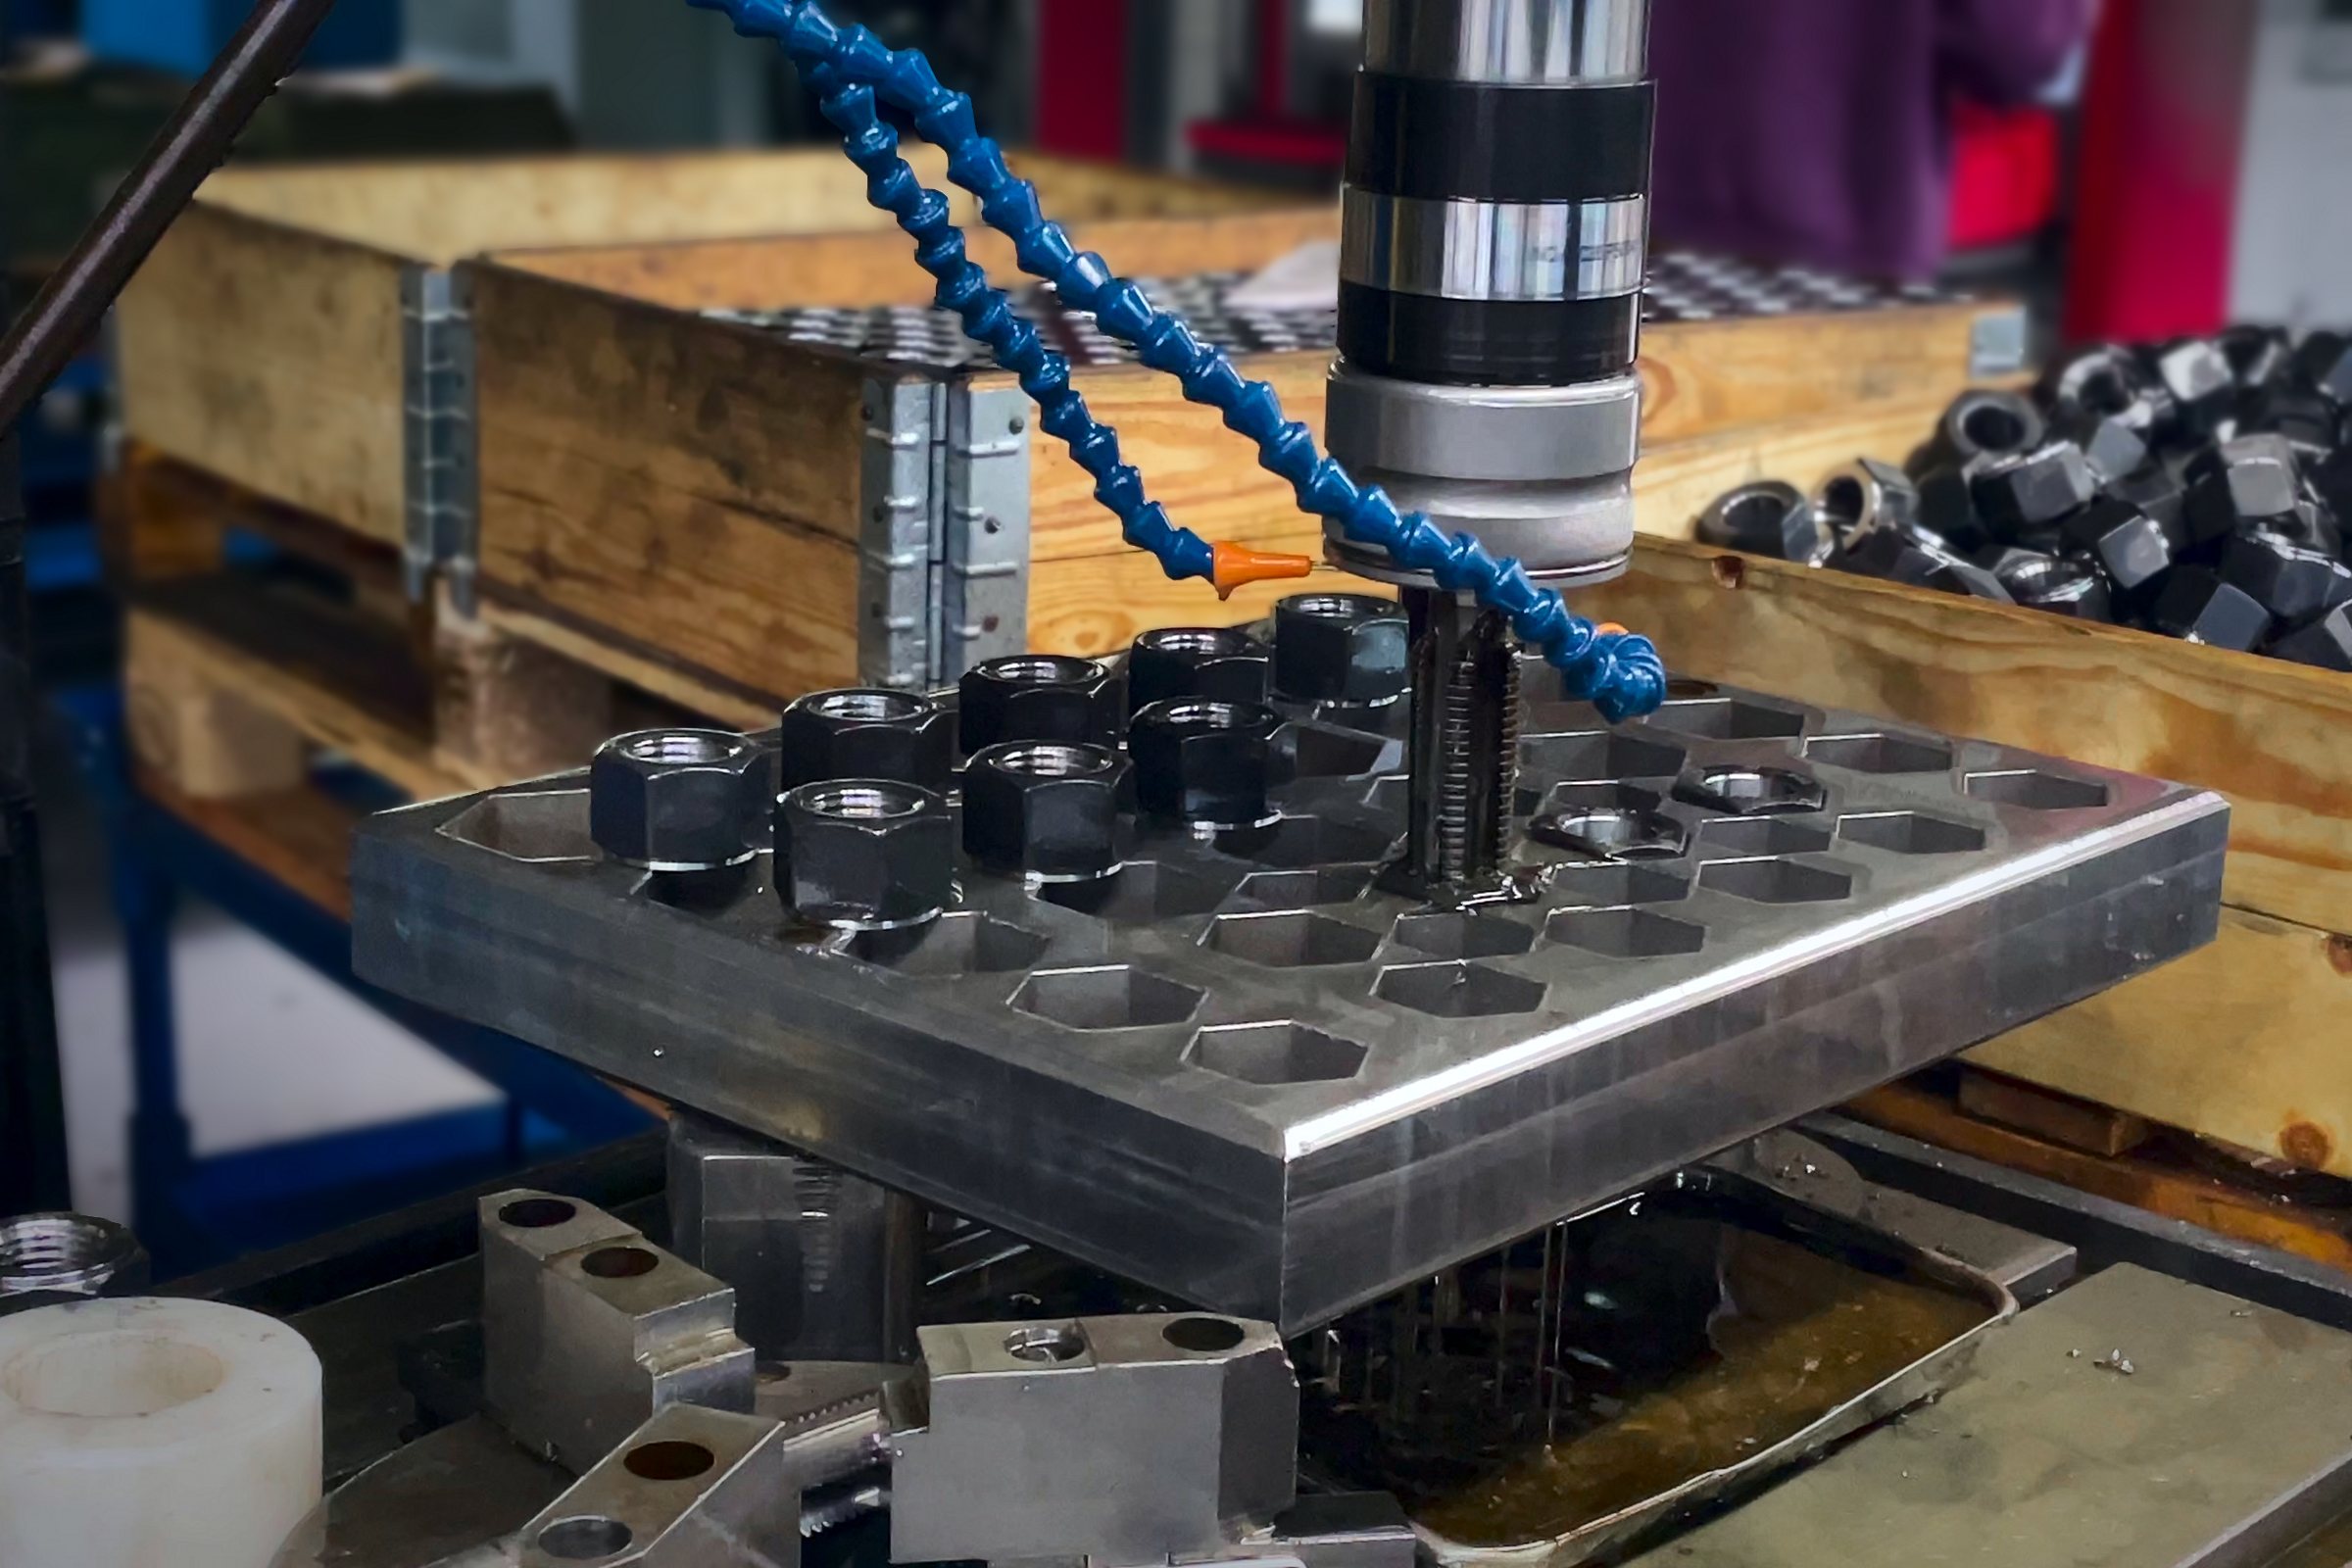
Special nuts are forged, pierced and finish-machined in-house. Internal threads are produced on our own tapping machines, typically up to M80, larger sizes on request with turned threads, including heavy hex to ASME. Every nut carries the RS manufacturer’s mark and matches the bolt from the same production.
08
Surface treatment
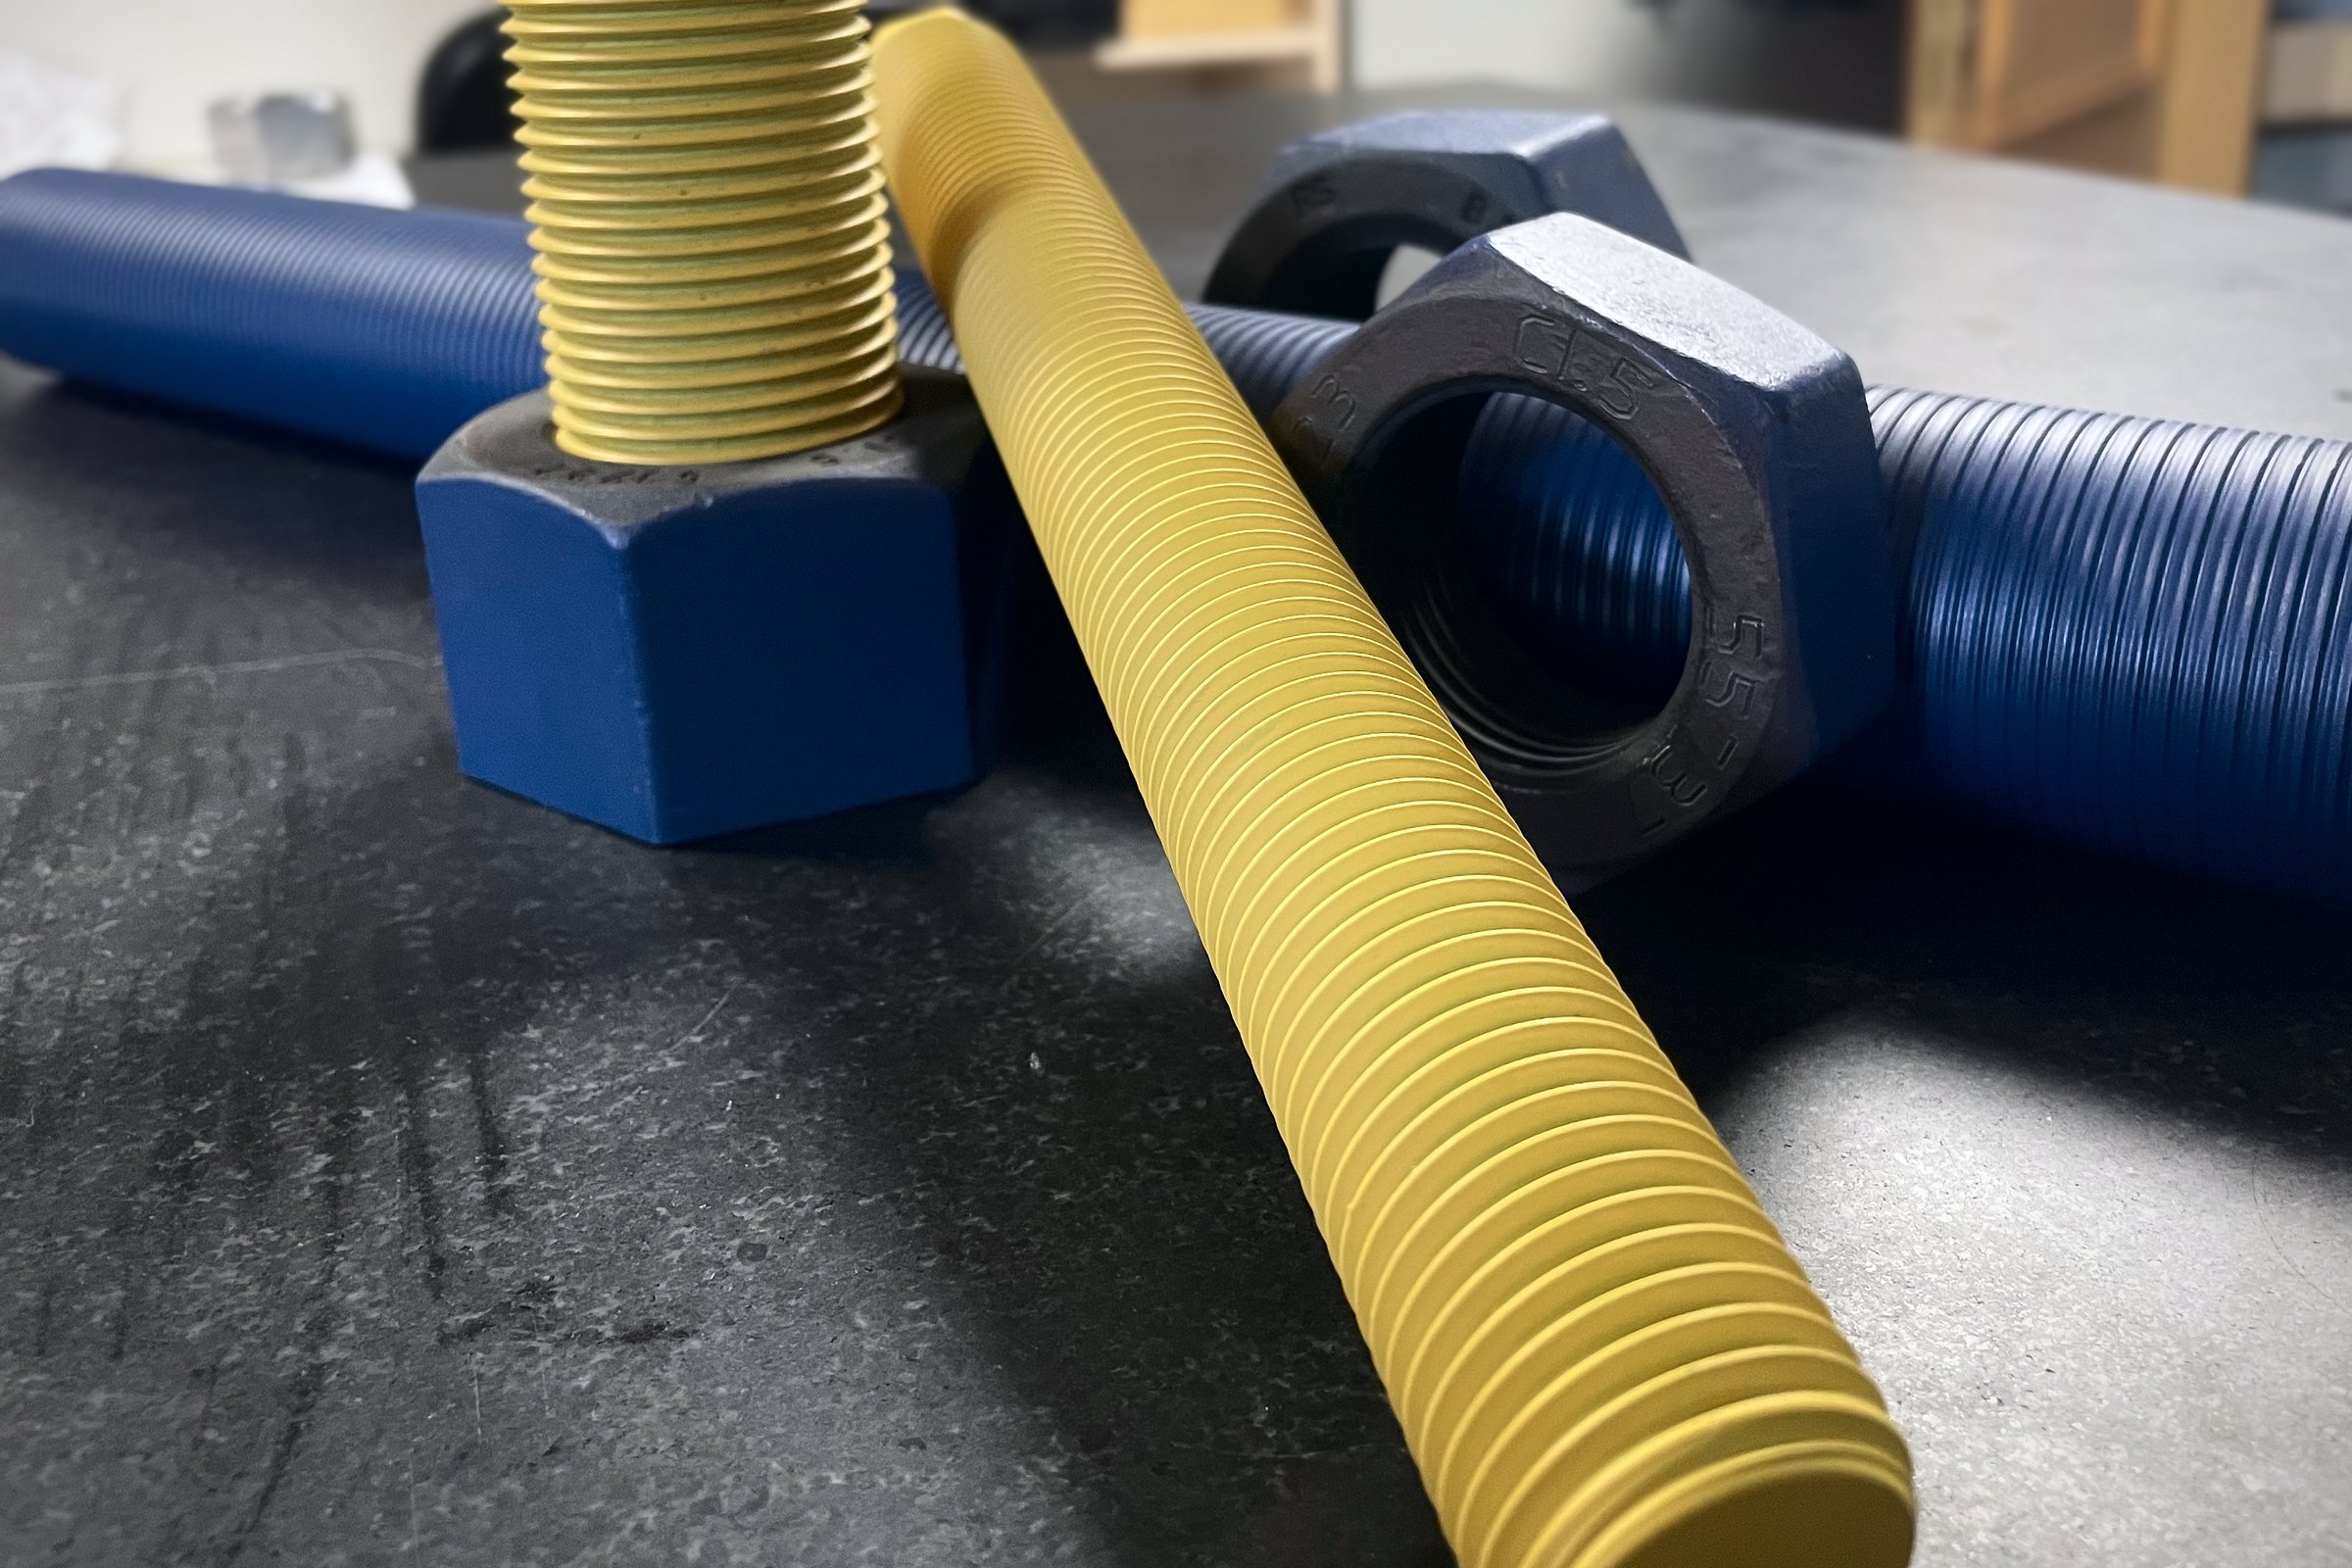
More than 50 coatings through long-standing partners, from electroplated zinc and zinc flake systems to anti-friction coatings over manganese phosphate. Inspection stays in-house: coating thickness, cross-section and thread gauging. High-strength parts are baked after electroplating to prevent hydrogen embrittlement.
09
Testing and materials laboratory
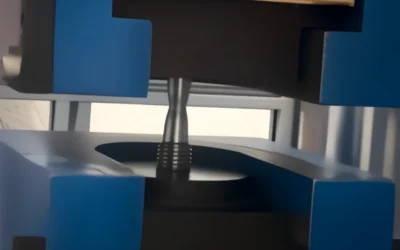
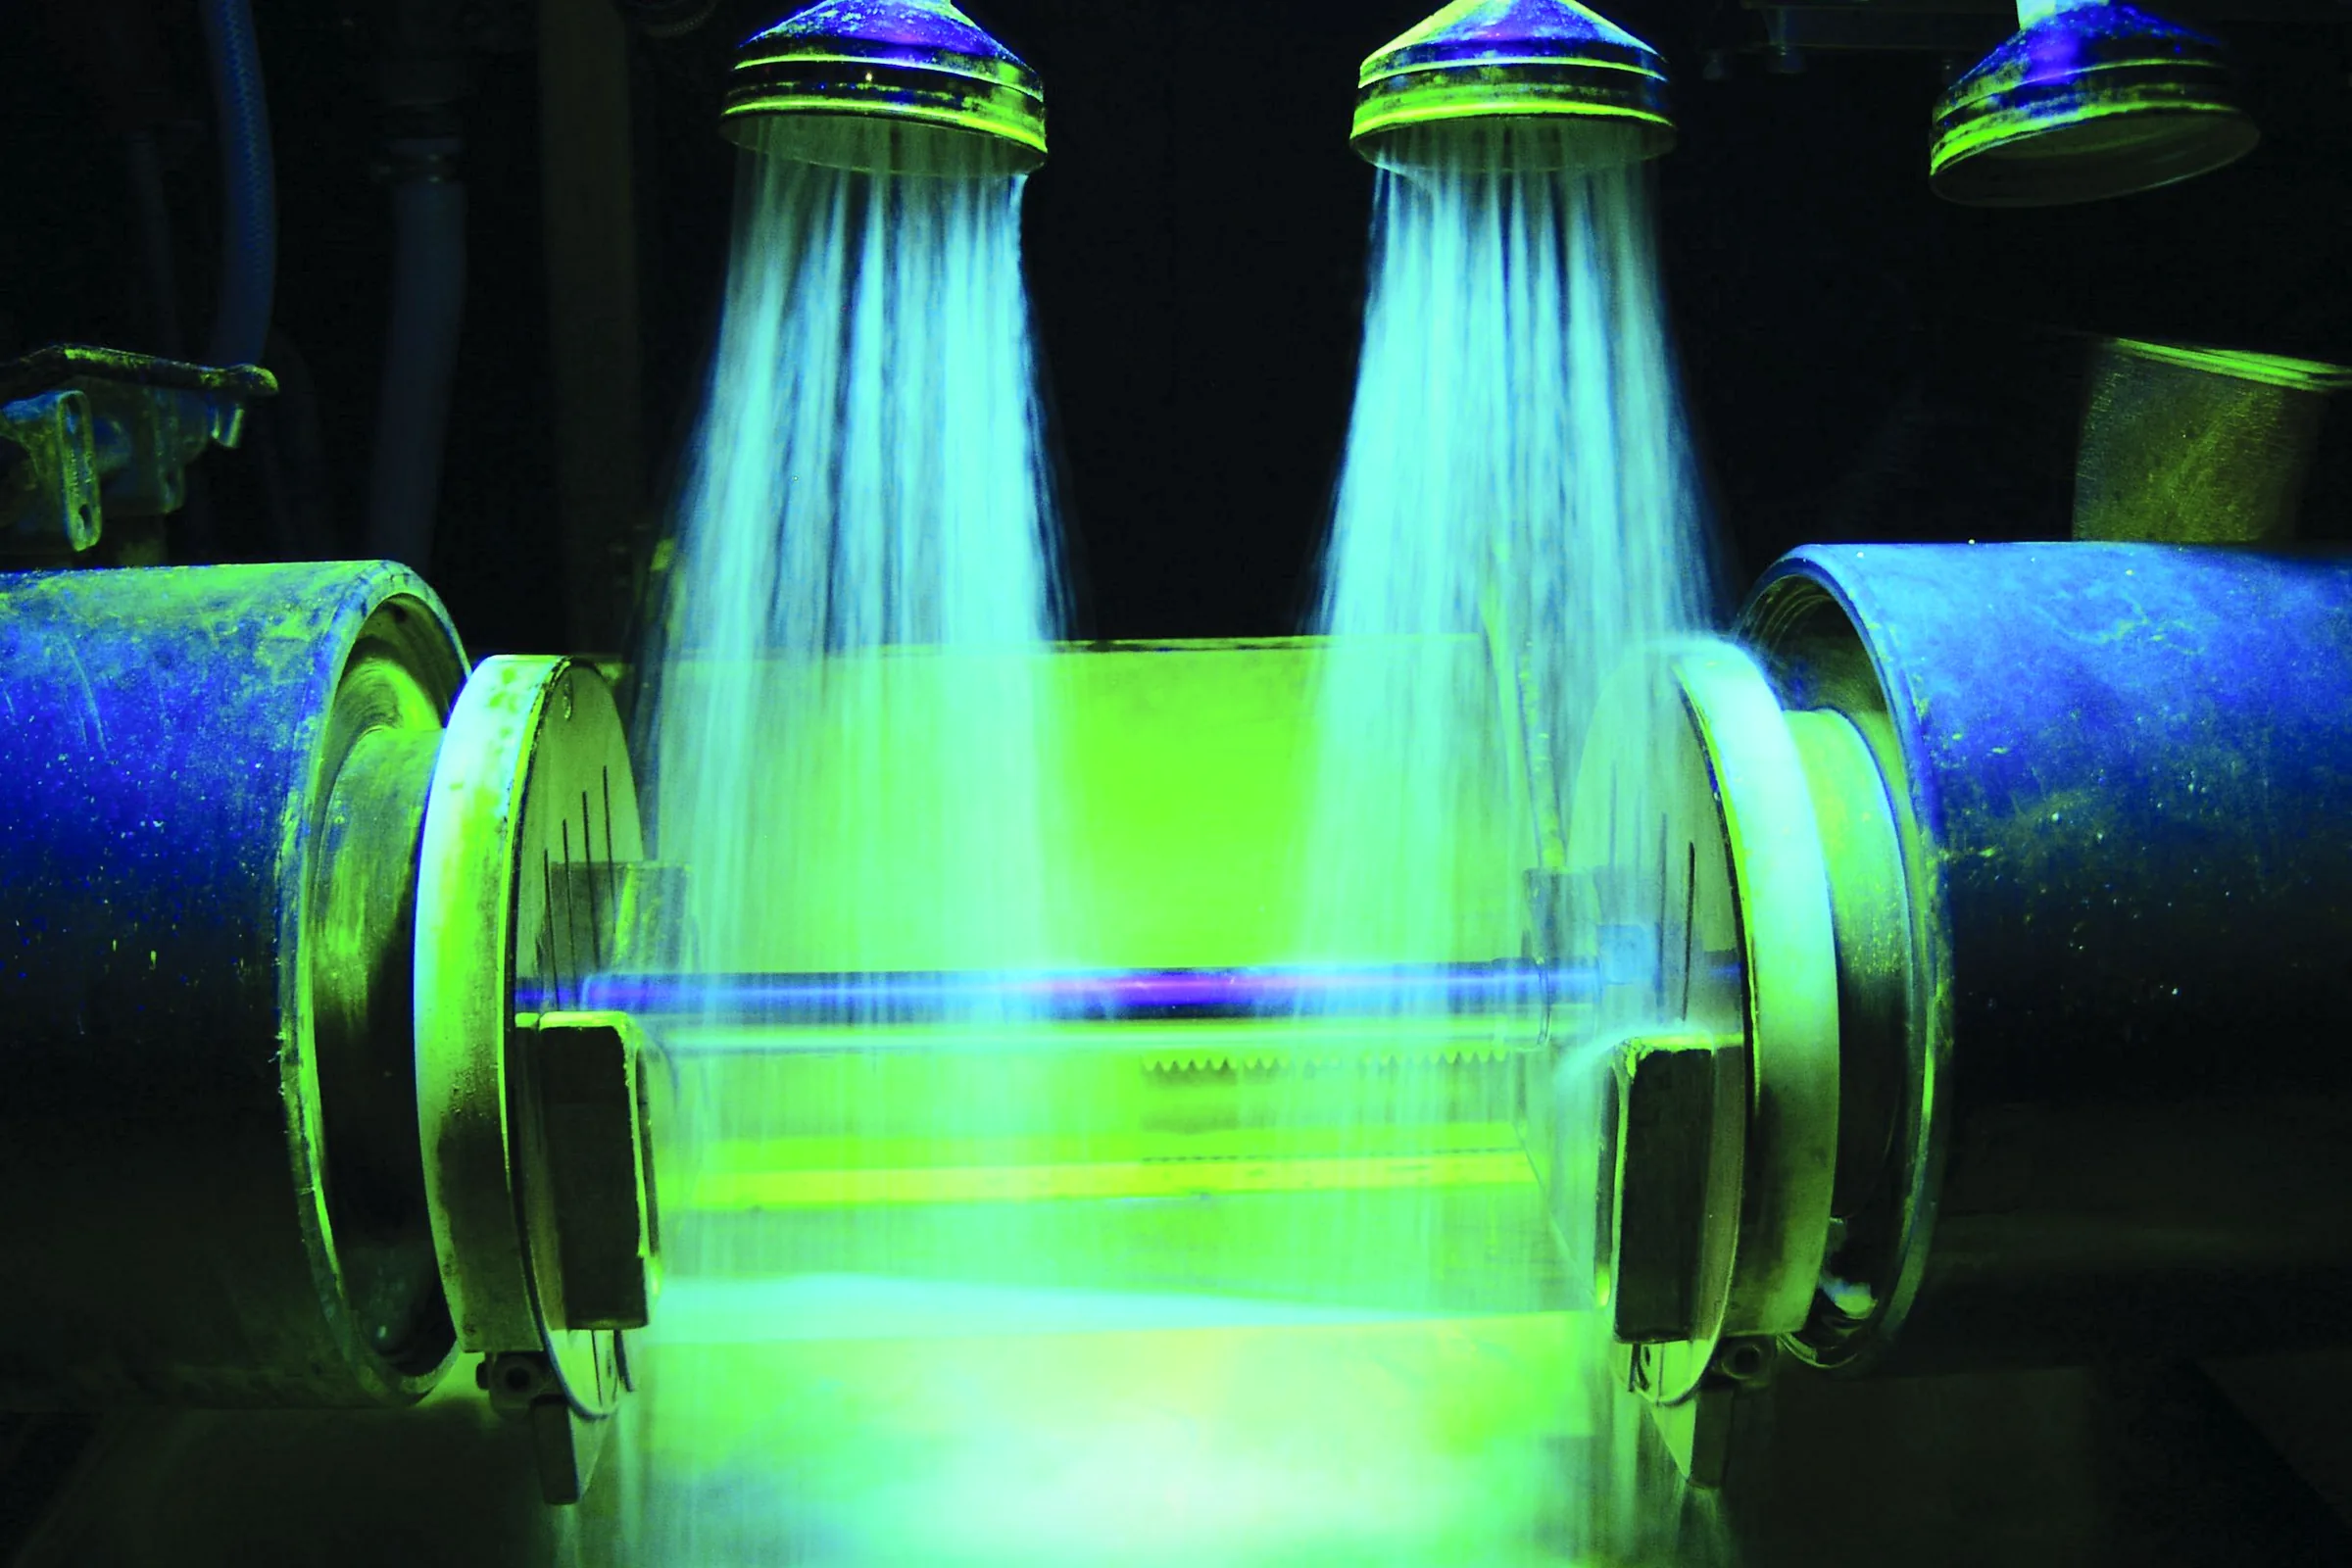
Our in-house materials laboratory is our key differentiator: tensile testing on the full-size bolt up to 3,000 kN, Charpy impact testing in-house down to –70 °C and through accredited partners down to –196 °C, hardness testing, chemical analysis, bend testing, micro- and macro-etch examination. Non-destructive testing by magnetic particle, dye penetrant, ultrasonic and visual testing, carried out by inspectors certified to ISO 9712 Level 2. We also provide materials testing as a service.
10
Shipping
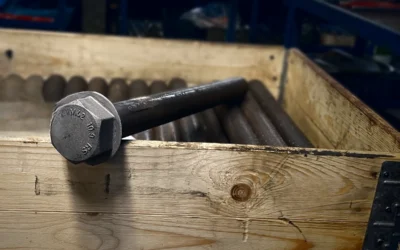
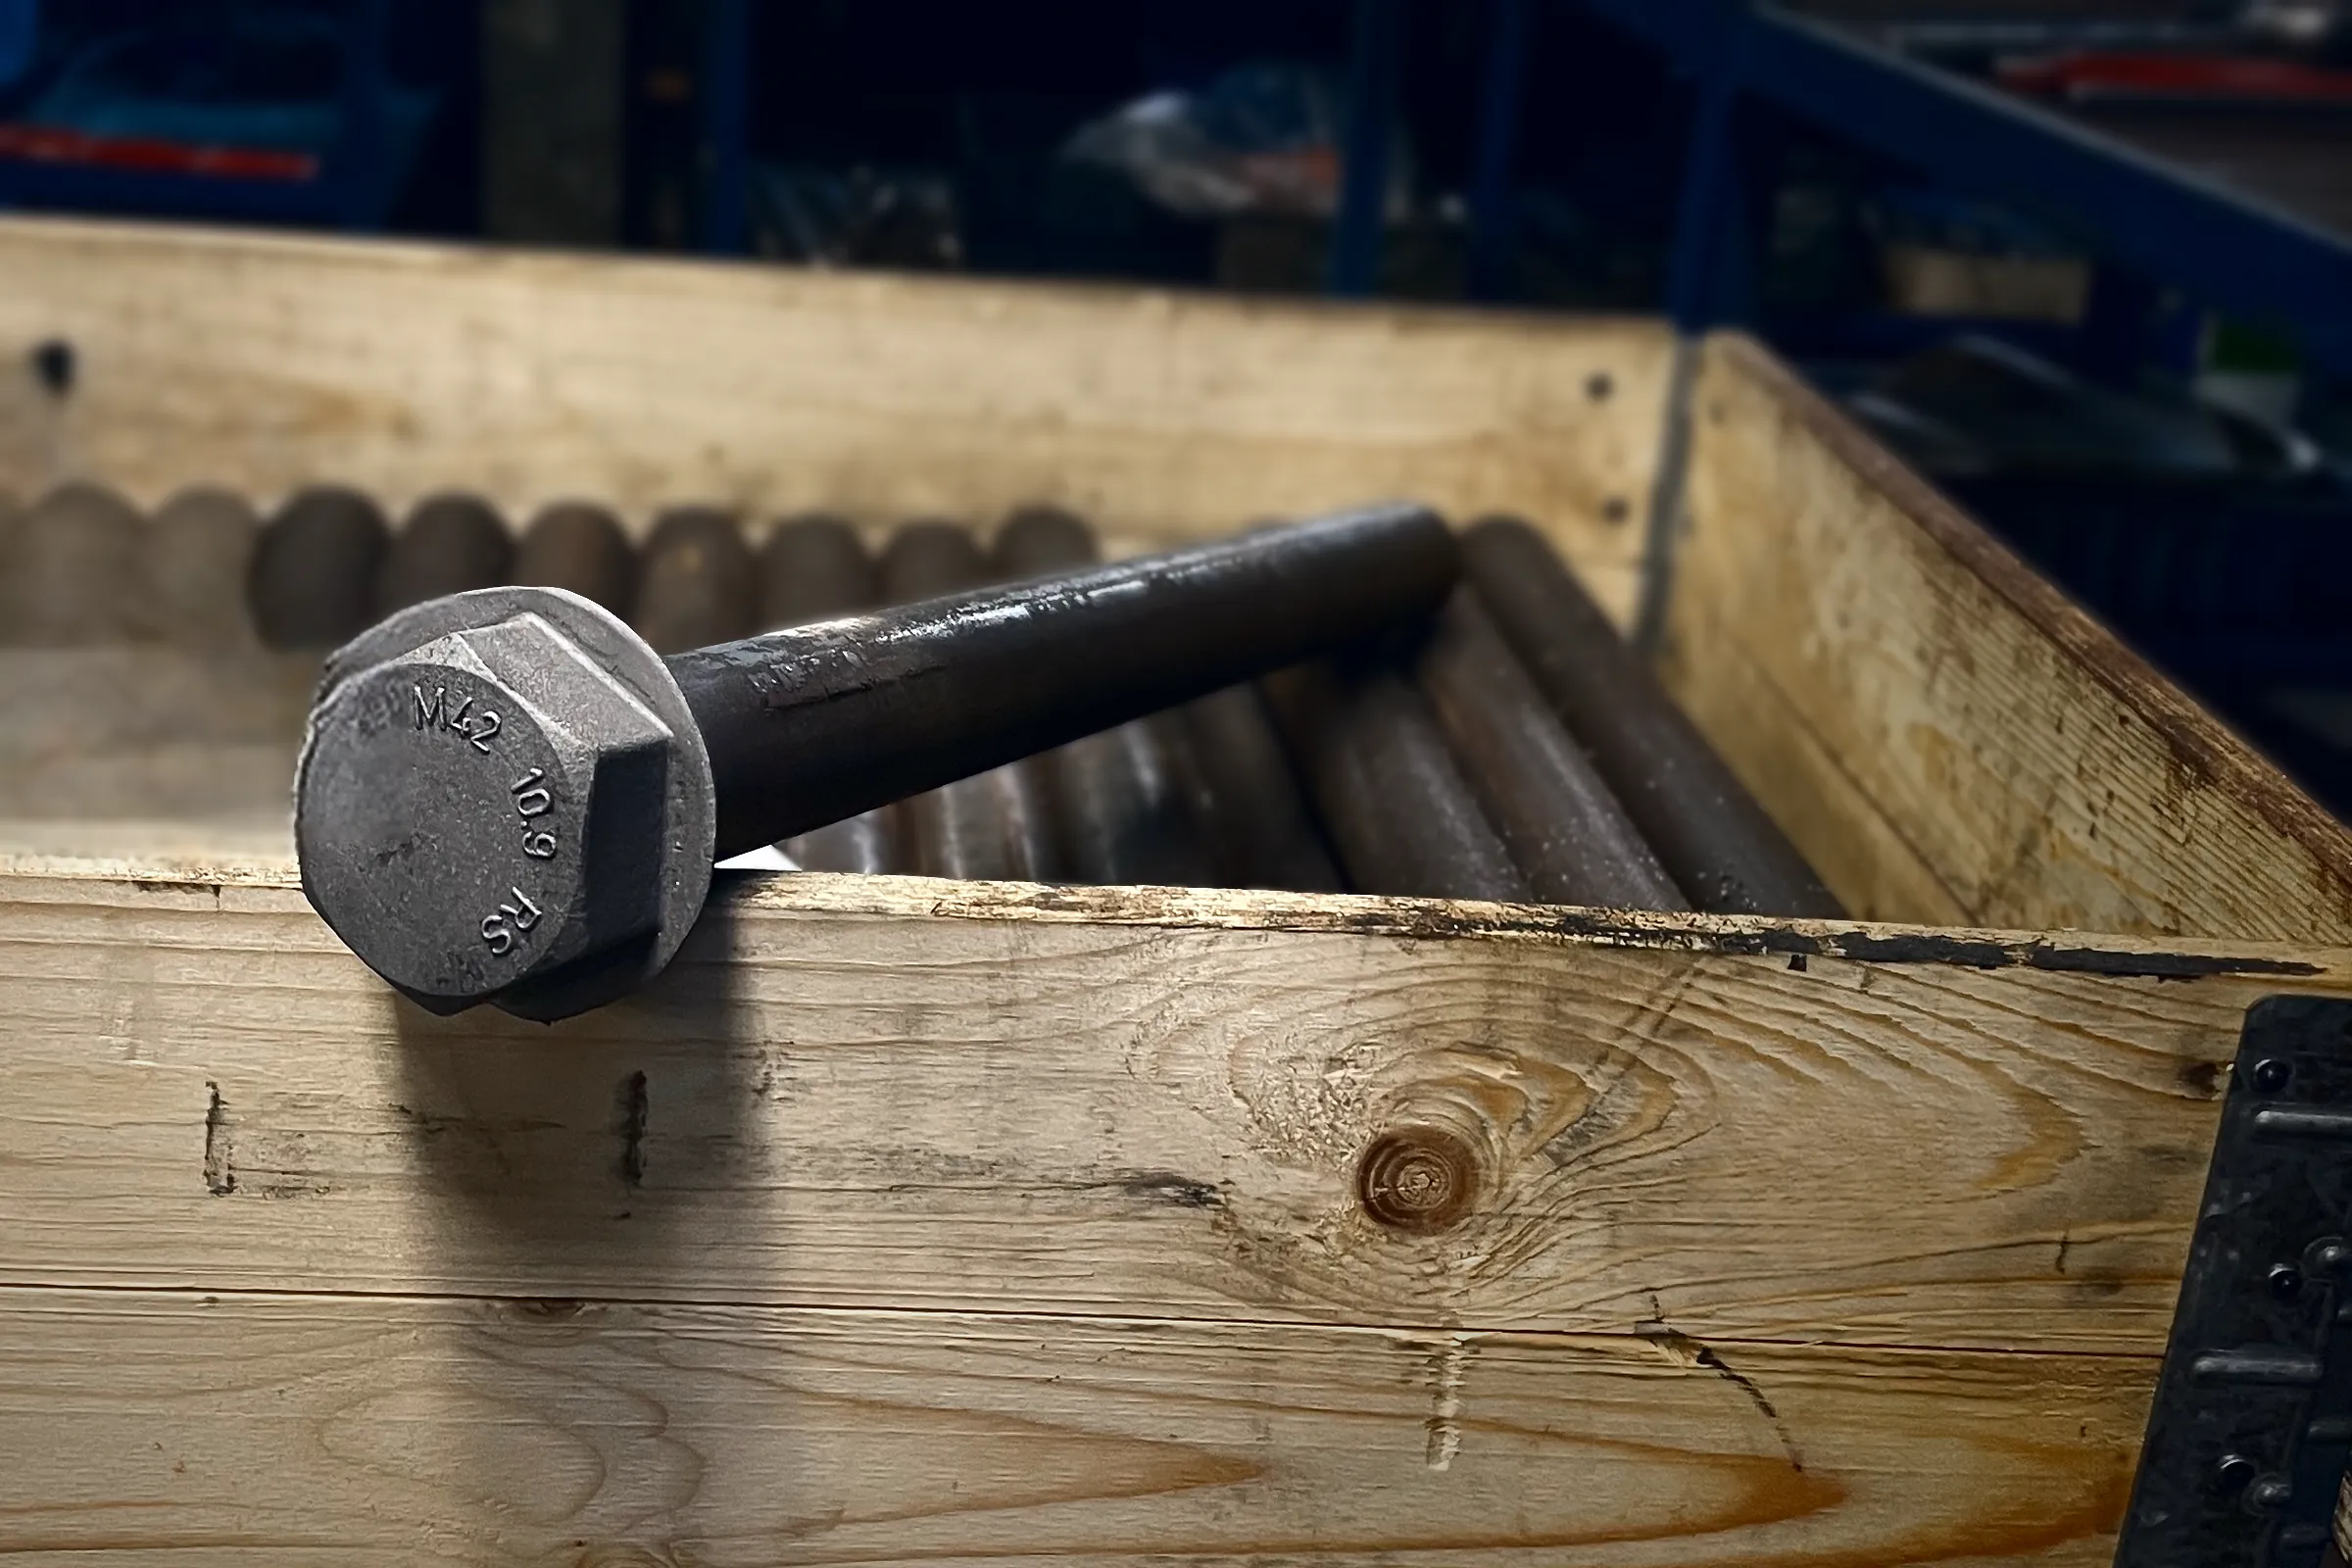
Packing depends on weight and sensitivity: carton, wooden crate, mesh box or pallet, fine threads protected, corrosion protection on request. Different batches never go into the same container; each batch stays segregated, all the way into the box. On request, we deliver in neutral packaging.
Send us your enquiry for special fasteners to standard or drawing
Urgent? You will hear from us within a few hours.
Inside our production
Production gallery