
Knowledge base
Die-sinking EDM explained simply
Producing shapes in hardened steel without cutting
Term explained
Producing shapes in hardened steel without cutting
Die-sinking EDM is a material removal process that works without a cutting edge. An electrode made of copper or graphite, which carries the negative of the required shape, is brought to within a tiny gap of the workpiece in a non-conductive bath. Thousands of small sparks jump between the two, each one melting and vaporising a tiny particle of steel. In this way, the electrode sinks into the workpiece and leaves its shape behind, even in hardened steel that could no longer be milled. Because there are no cutting forces, even delicate and deep contours are produced with dimensional accuracy.
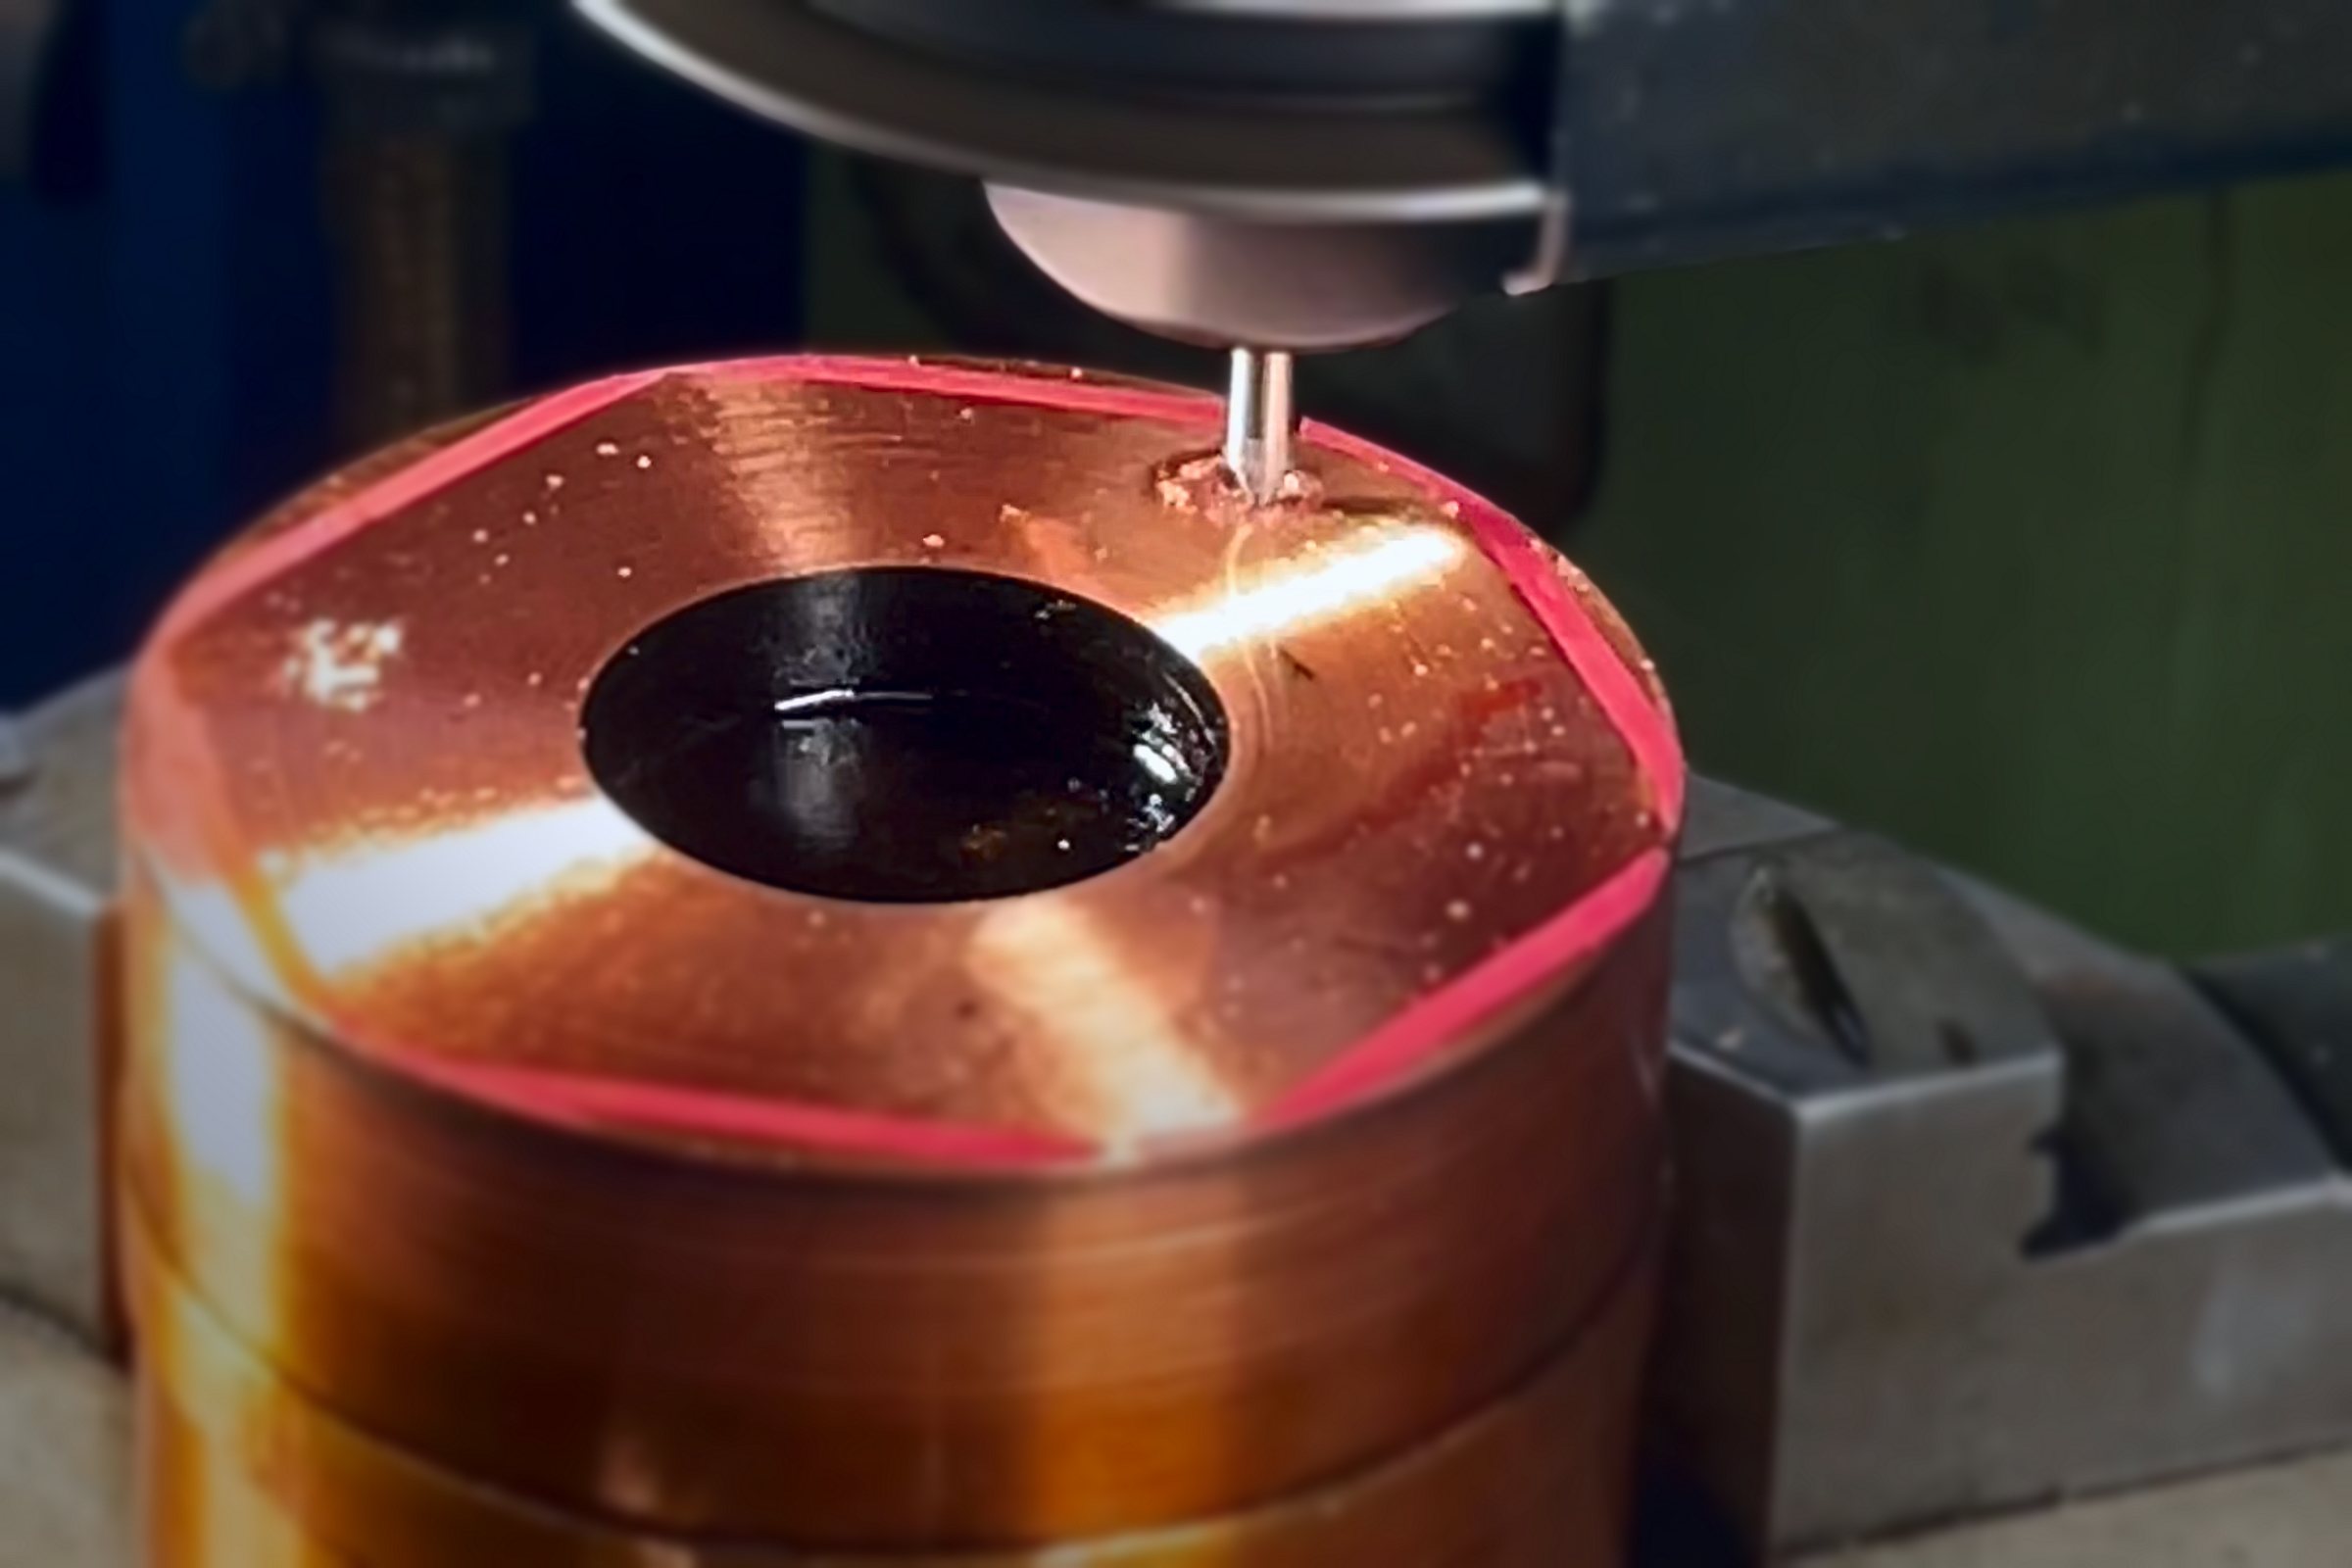
What RS Randack uses EDM for
- Dies for the forge: The impressions of the forging dies for heads, collars and special shapes are produced by EDM in our own toolroom. A new die for a part made to drawing is therefore made in-house, without waiting for a tool supplier.
- Internal contours in bolts: Hexagon sockets, internal serrations and special profiles in heads, particularly for small quantities and in high-strength or stainless materials.
- Contract EDM for third parties: Toolmakers, machine builders and maintenance companies have shapes, openings and repairs on hardened parts produced by EDM, with in-house electrode manufacture on lathe and milling machine.
How we work
Electrodes are made in-house to drawing and archived, so that a repeat job years later produces the same shape. The first parts of a series are fully measured, followed by sample checks. Several EDM machines are available, so toolmaking and contract jobs can run in parallel.
What you should specify
Drawing or 3D data of the contour, material and hardness of the workpiece, depth and surface finish, quantity, whether the electrode should be kept for repeat orders.
Enquire about EDM work and tooling
Urgent? You will hear from us within a few hours.