
Production
Nut machining
Special nuts from the same production as the bolt
Step 7
Special nuts from the same production as the bolt
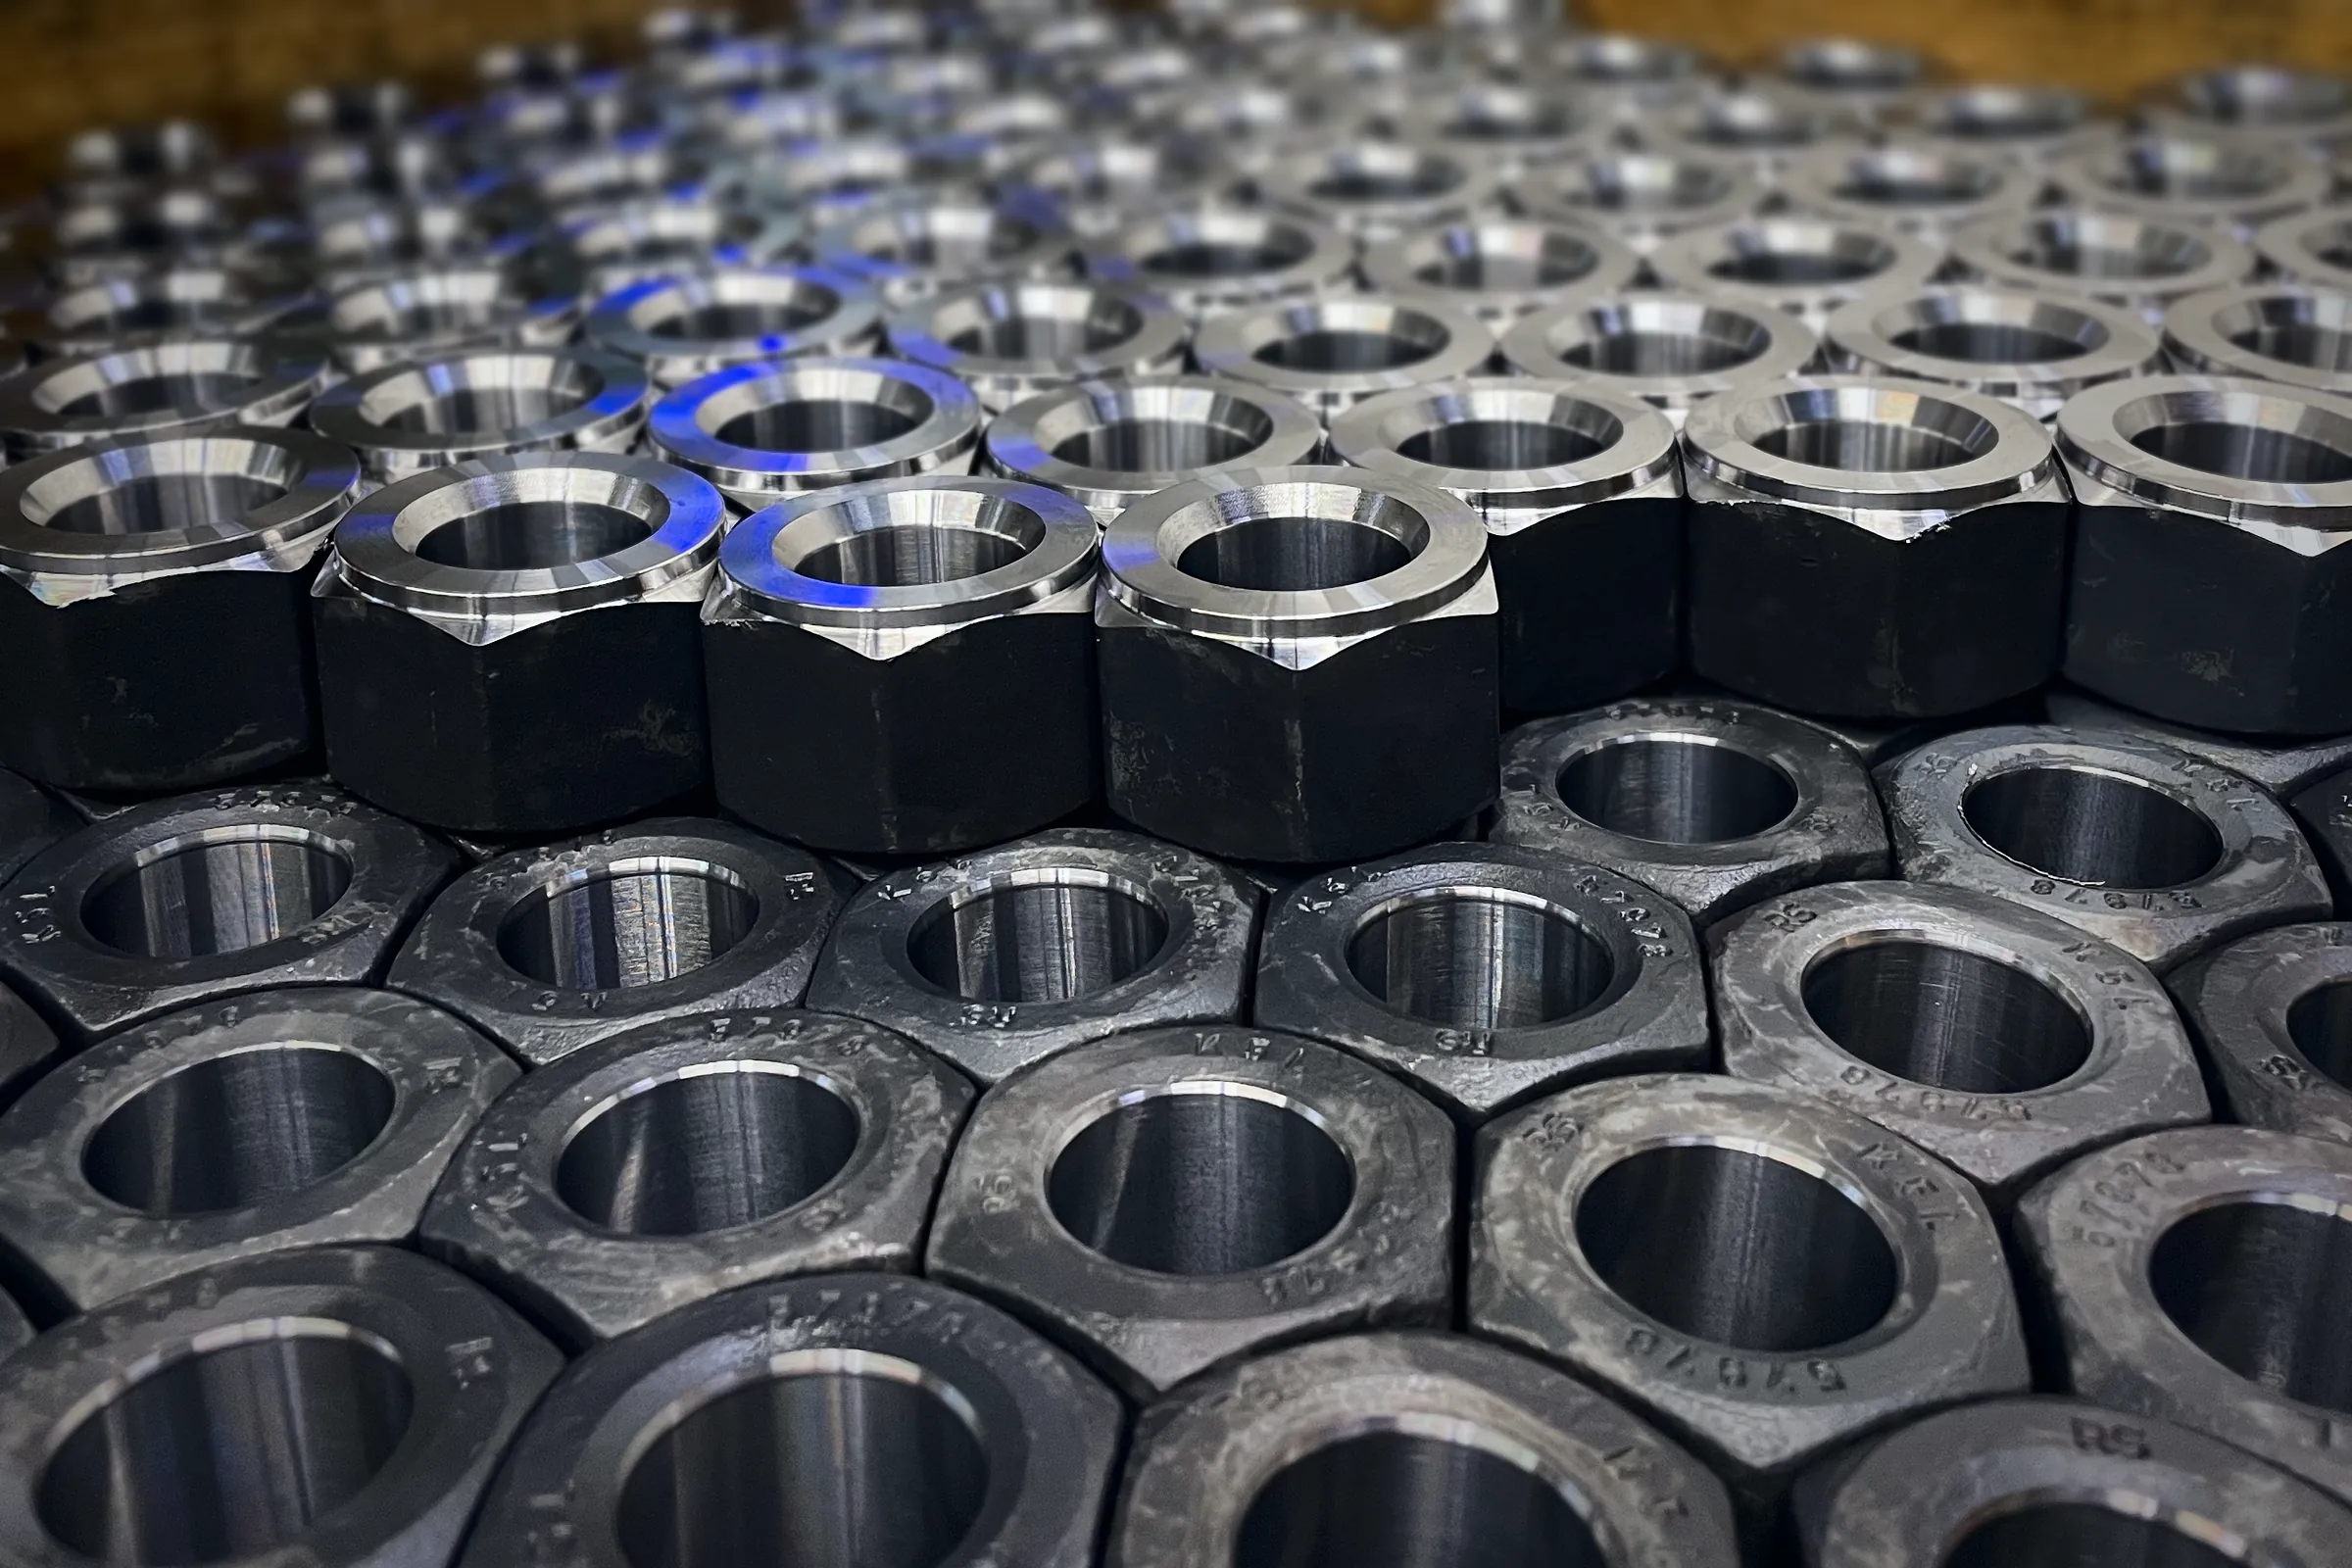
Every special bolt needs a matching nut. RS Randack produces hex nuts, heavy hex nuts to ASME, cap nuts, nuts to DIN 2510, slotted round nuts and special shapes to drawing in-house: the blank is hot-preformed and hot-pierced in our own forge, finish-machined on the CNC turning centres after heat treatment and given a cut or turned internal thread, typically up to M80, larger sizes on request. Every nut carries the RS manufacturer’s mark.
M80
Internal threads, typically up to
2H
Heavy hex to ASME
8, 10, 12
Nut property classes
Why RS Randack nuts are pierced, not drilled
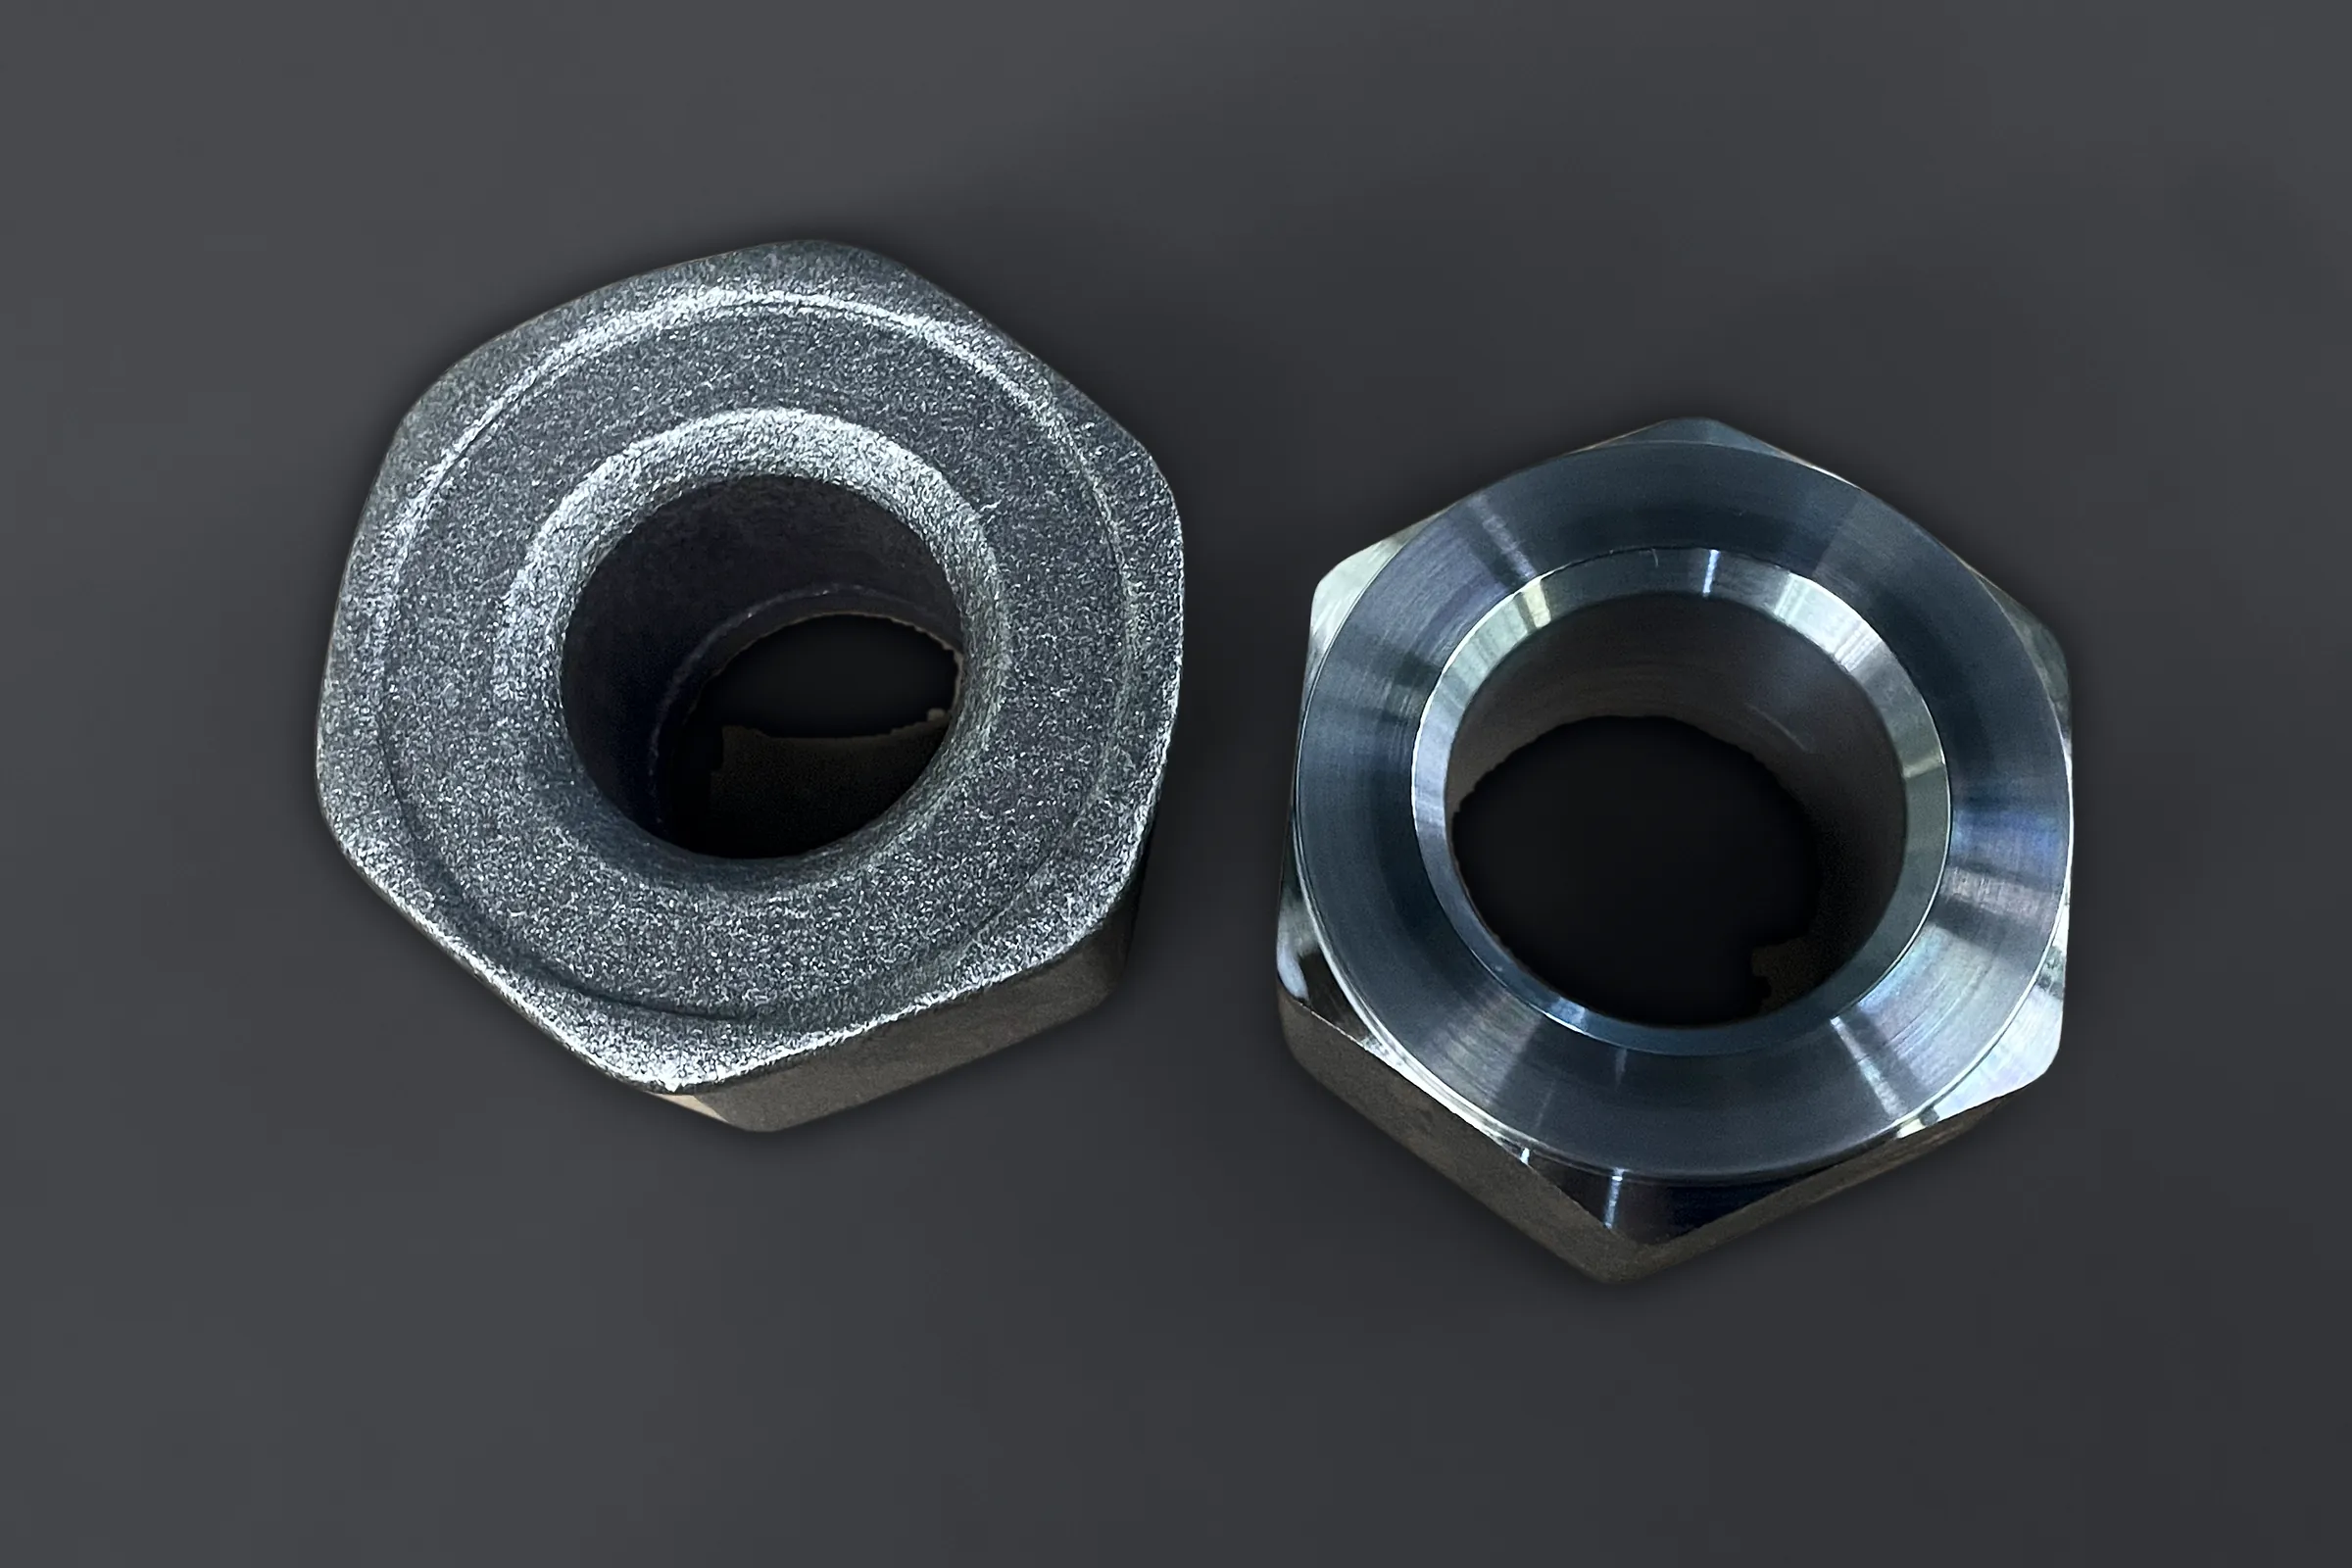
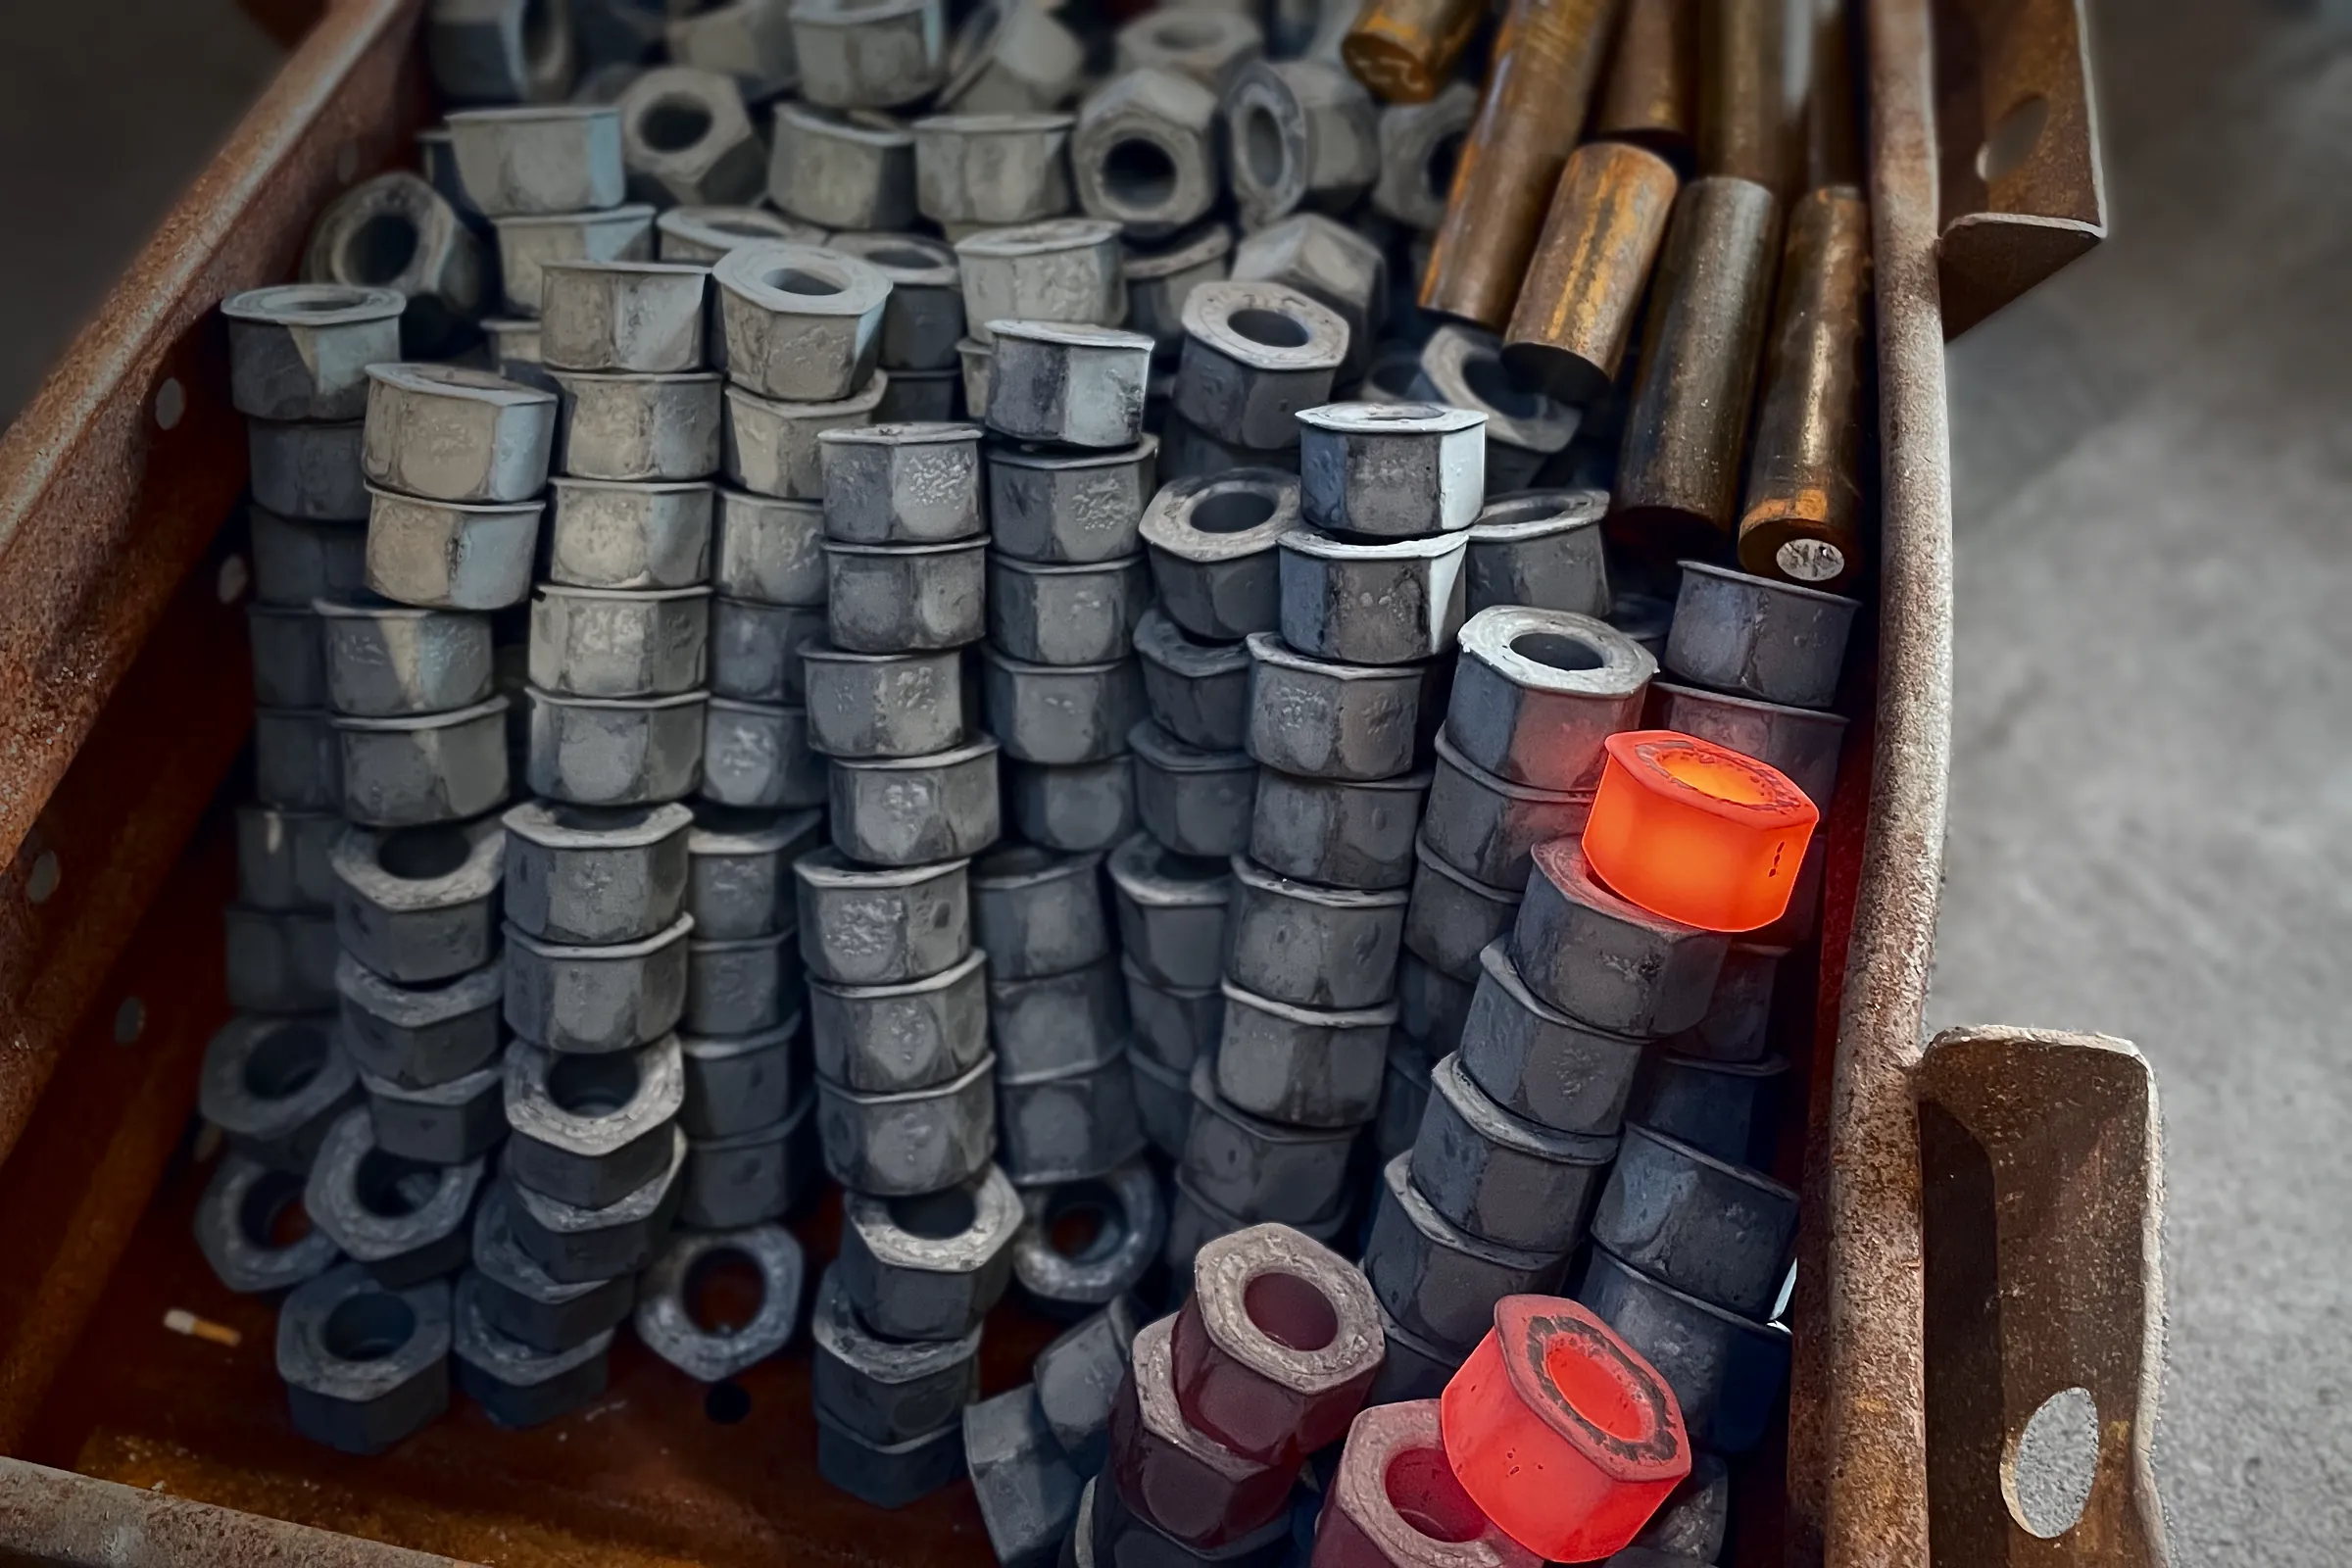
Drilling a large nut from hexagon bar wastes material and cuts through the grain flow. During piercing in the forge, the piercing punch displaces the core of the red-hot blank; the material flows around the hole and the grain flow in the nut body is preserved. After forging, the nuts cool slowly so that the microstructure becomes uniform and they machine well.
Which nuts we produce
- Hex nuts to ISO 4032, DIN 934 and to drawing, in high and thin types
- Heavy hex nuts to ASME B18.2.2 in grades such as ASTM A194 2H, 4, 7 and 8 for stud bolts in plant engineering
- Nuts and cap nuts to DIN 2510 for reduced-shank bolted joints
- Slotted round nuts, square nuts, collar nuts, nuts with spigots or holes to drawing
- Materials: Q&T steels, creep-resistant steels to EN 10269, stainless steels, duplex, nickel-based alloys and American grades, matched to the bolt
Which nut goes with which bolt
Under ISO 898-2, the nut property class corresponds to the first number of the bolt property class: class 8 for 8.8, class 10 for 10.9, class 12 for 12.9. The nut must be strong enough that, in the event of overload, the bolt fractures in the free threaded length rather than the nut thread stripping. For inch threads, a grade B7 stud bolt takes a grade 2H heavy hex nut, and grade L7 takes a grade 4 or 7 nut with low-temperature impact testing. For more on strength, see Property class 10.9; for inch threads, see American threads.
How the internal thread is produced
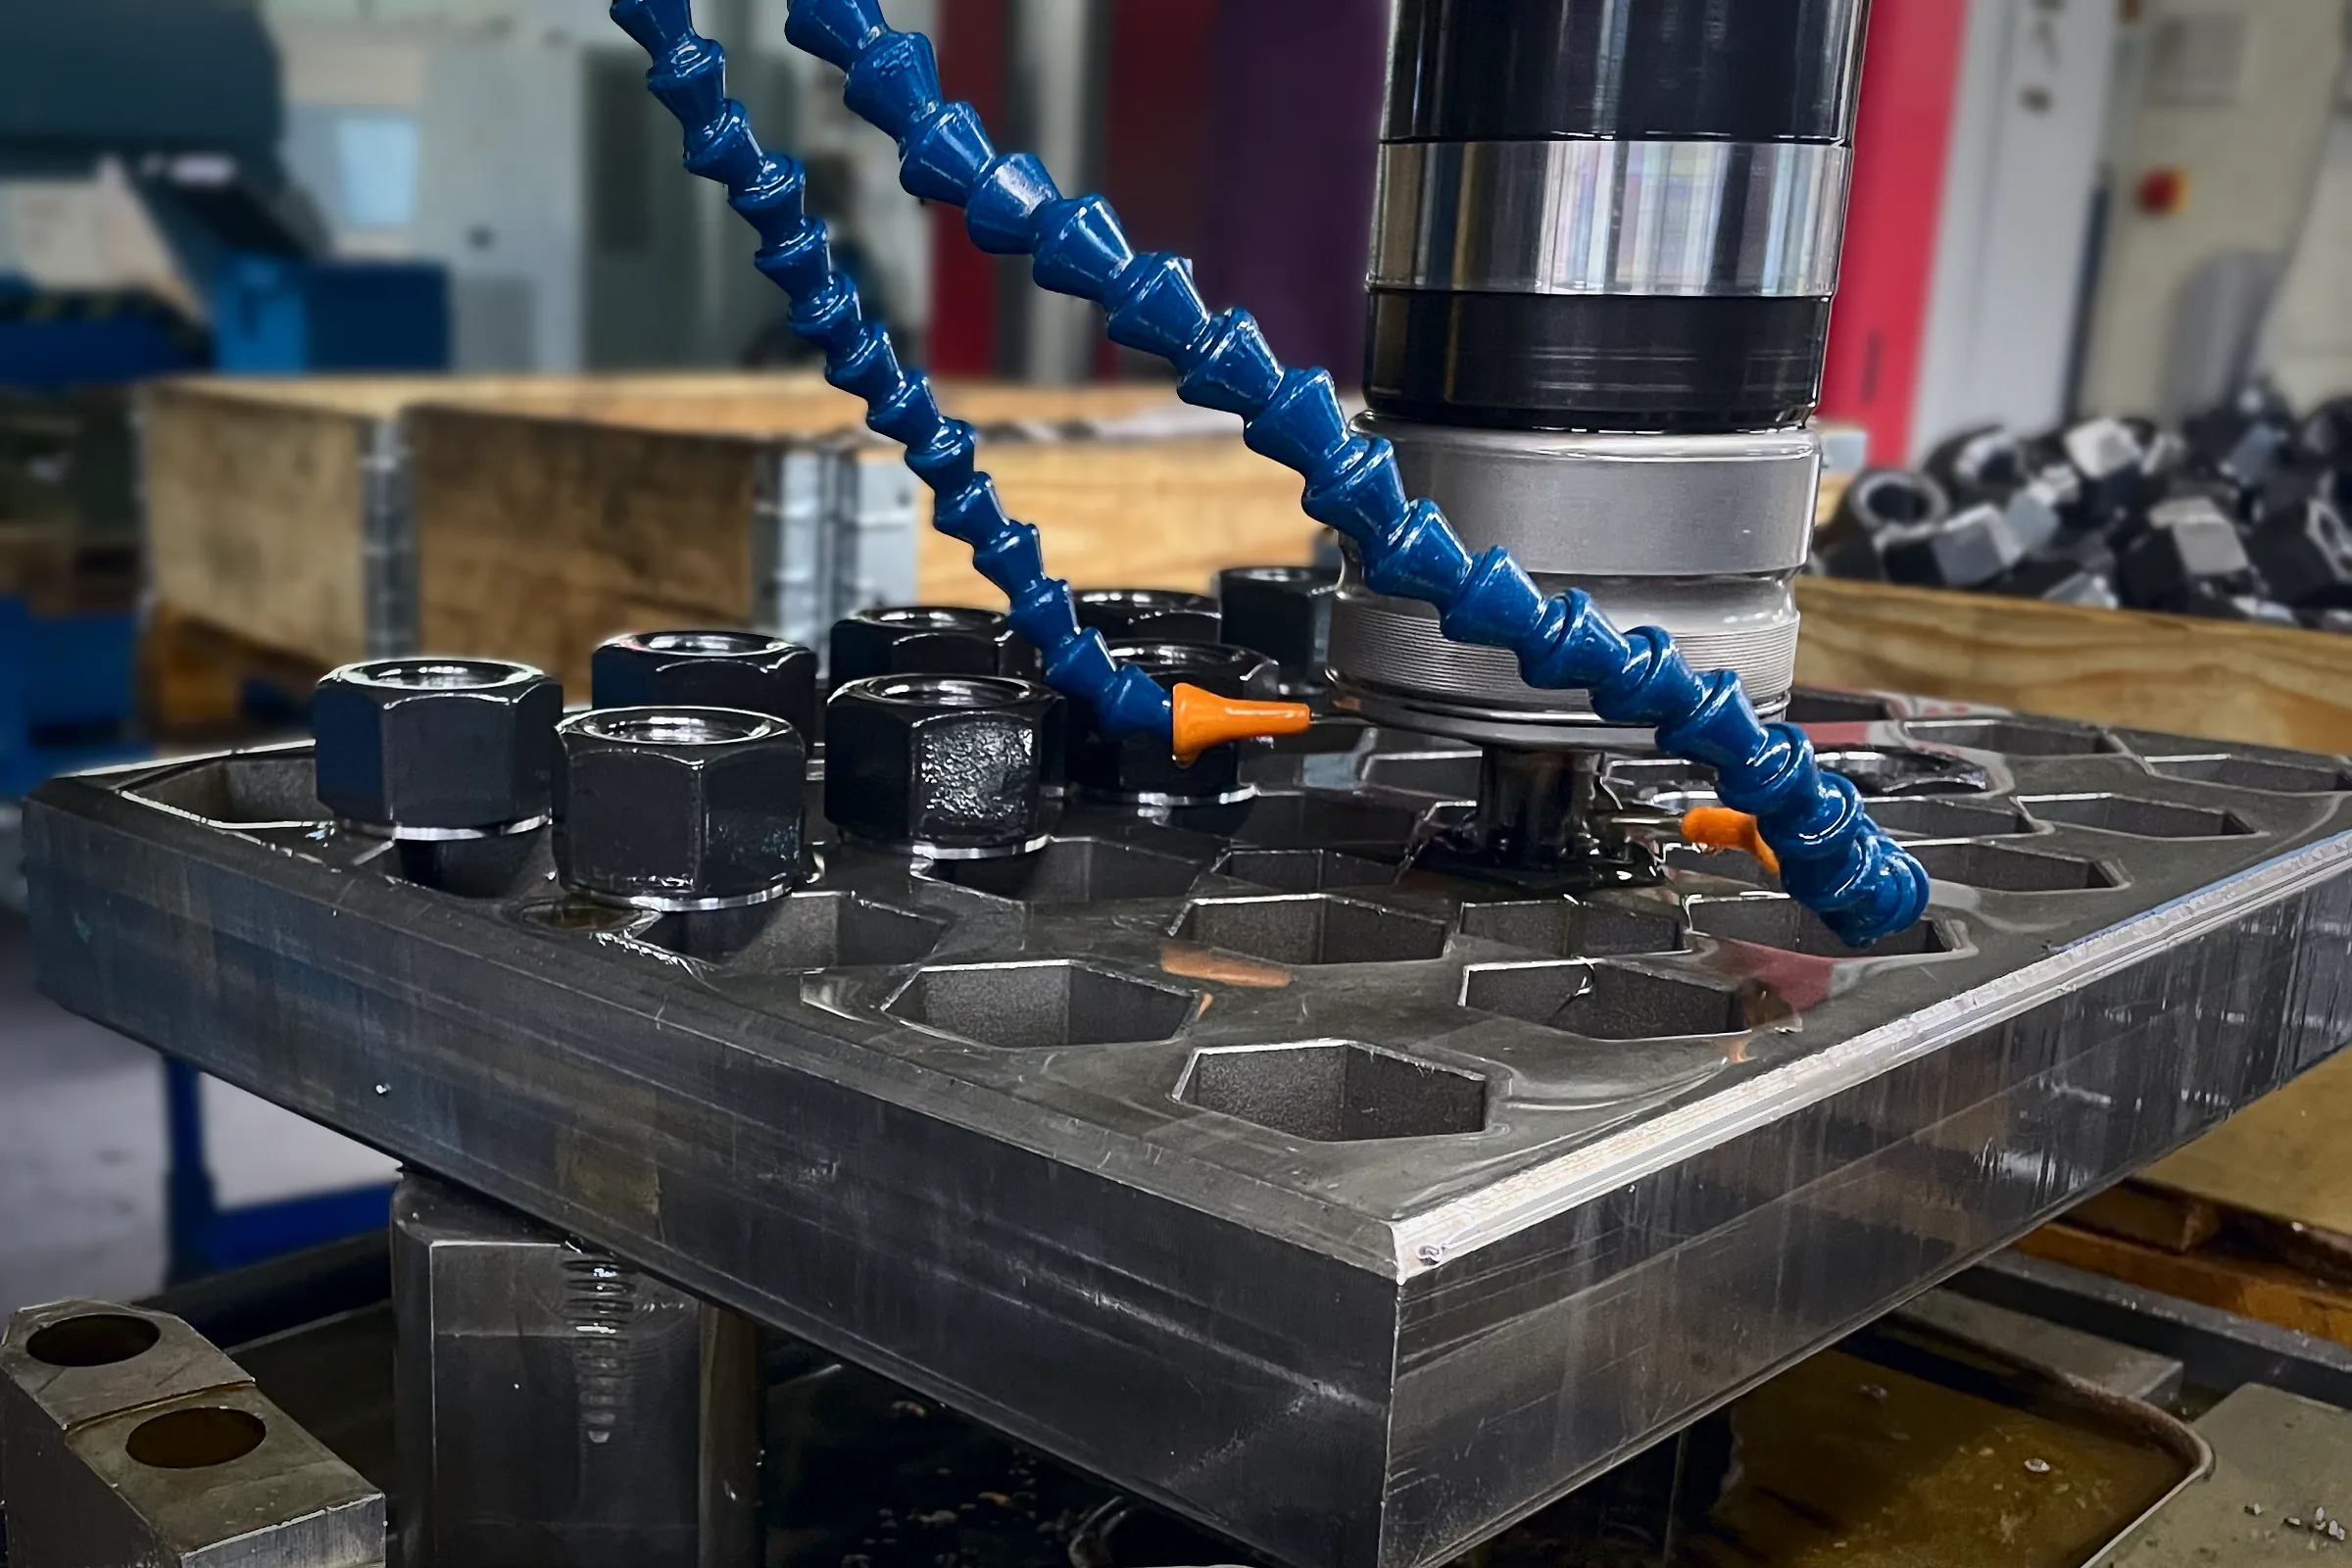
Internal threads are cut with taps on our own tapping machines, and turned on the turning centre for larger diameters. The standard fit is 6H with a 6g bolt; oversizes for coatings or special fits to drawing. Inspection is carried out with a thread plug gauge on the first parts and on samples, together with checks of height, width across flats and bearing-face runout. If the nut is to be coated, the thread is cut with an allowance so that the nut fits the bolt after coating.
Bolt and nut from a single source
If you order bolts and nuts from RS Randack, you get both in matched materials and batches, with matched tolerances, tested together and documented in the same certificate. For reduced-shank bolted joints, this includes spacer sleeves and cap nuts; for flanged joints, stud bolts with two heavy hex nuts.
Frequently asked questions
Questions and answers about nut machining
What is the maximum nut size RS Randack can produce?
Internal threads are typically cut up to M80, larger nuts on request with turned threads. Widths across flats and heights to standard or drawing.
Does RS Randack produce heavy hex nuts?
Yes, to ASME B18.2.2 in grades such as ASTM A194 2H, with UNC or 8UN inch threads, optionally with zinc flake or anti-friction coating and a 3.1 or 3.2 inspection certificate.
Can I order nuts only, without bolts?
Yes. Special nuts to drawing are also produced on their own, in lots from a few pieces to several thousand.
Enquire about special nuts to match your bolts
Urgent? You will hear from us within a few hours.