
Knowledge base
Zinc electroplating to ISO 4042
The classic coating up to 8.8, and why it needs approval for 10.9
Term explained
The classic coating up to 8.8, and why it needs approval for 10.9
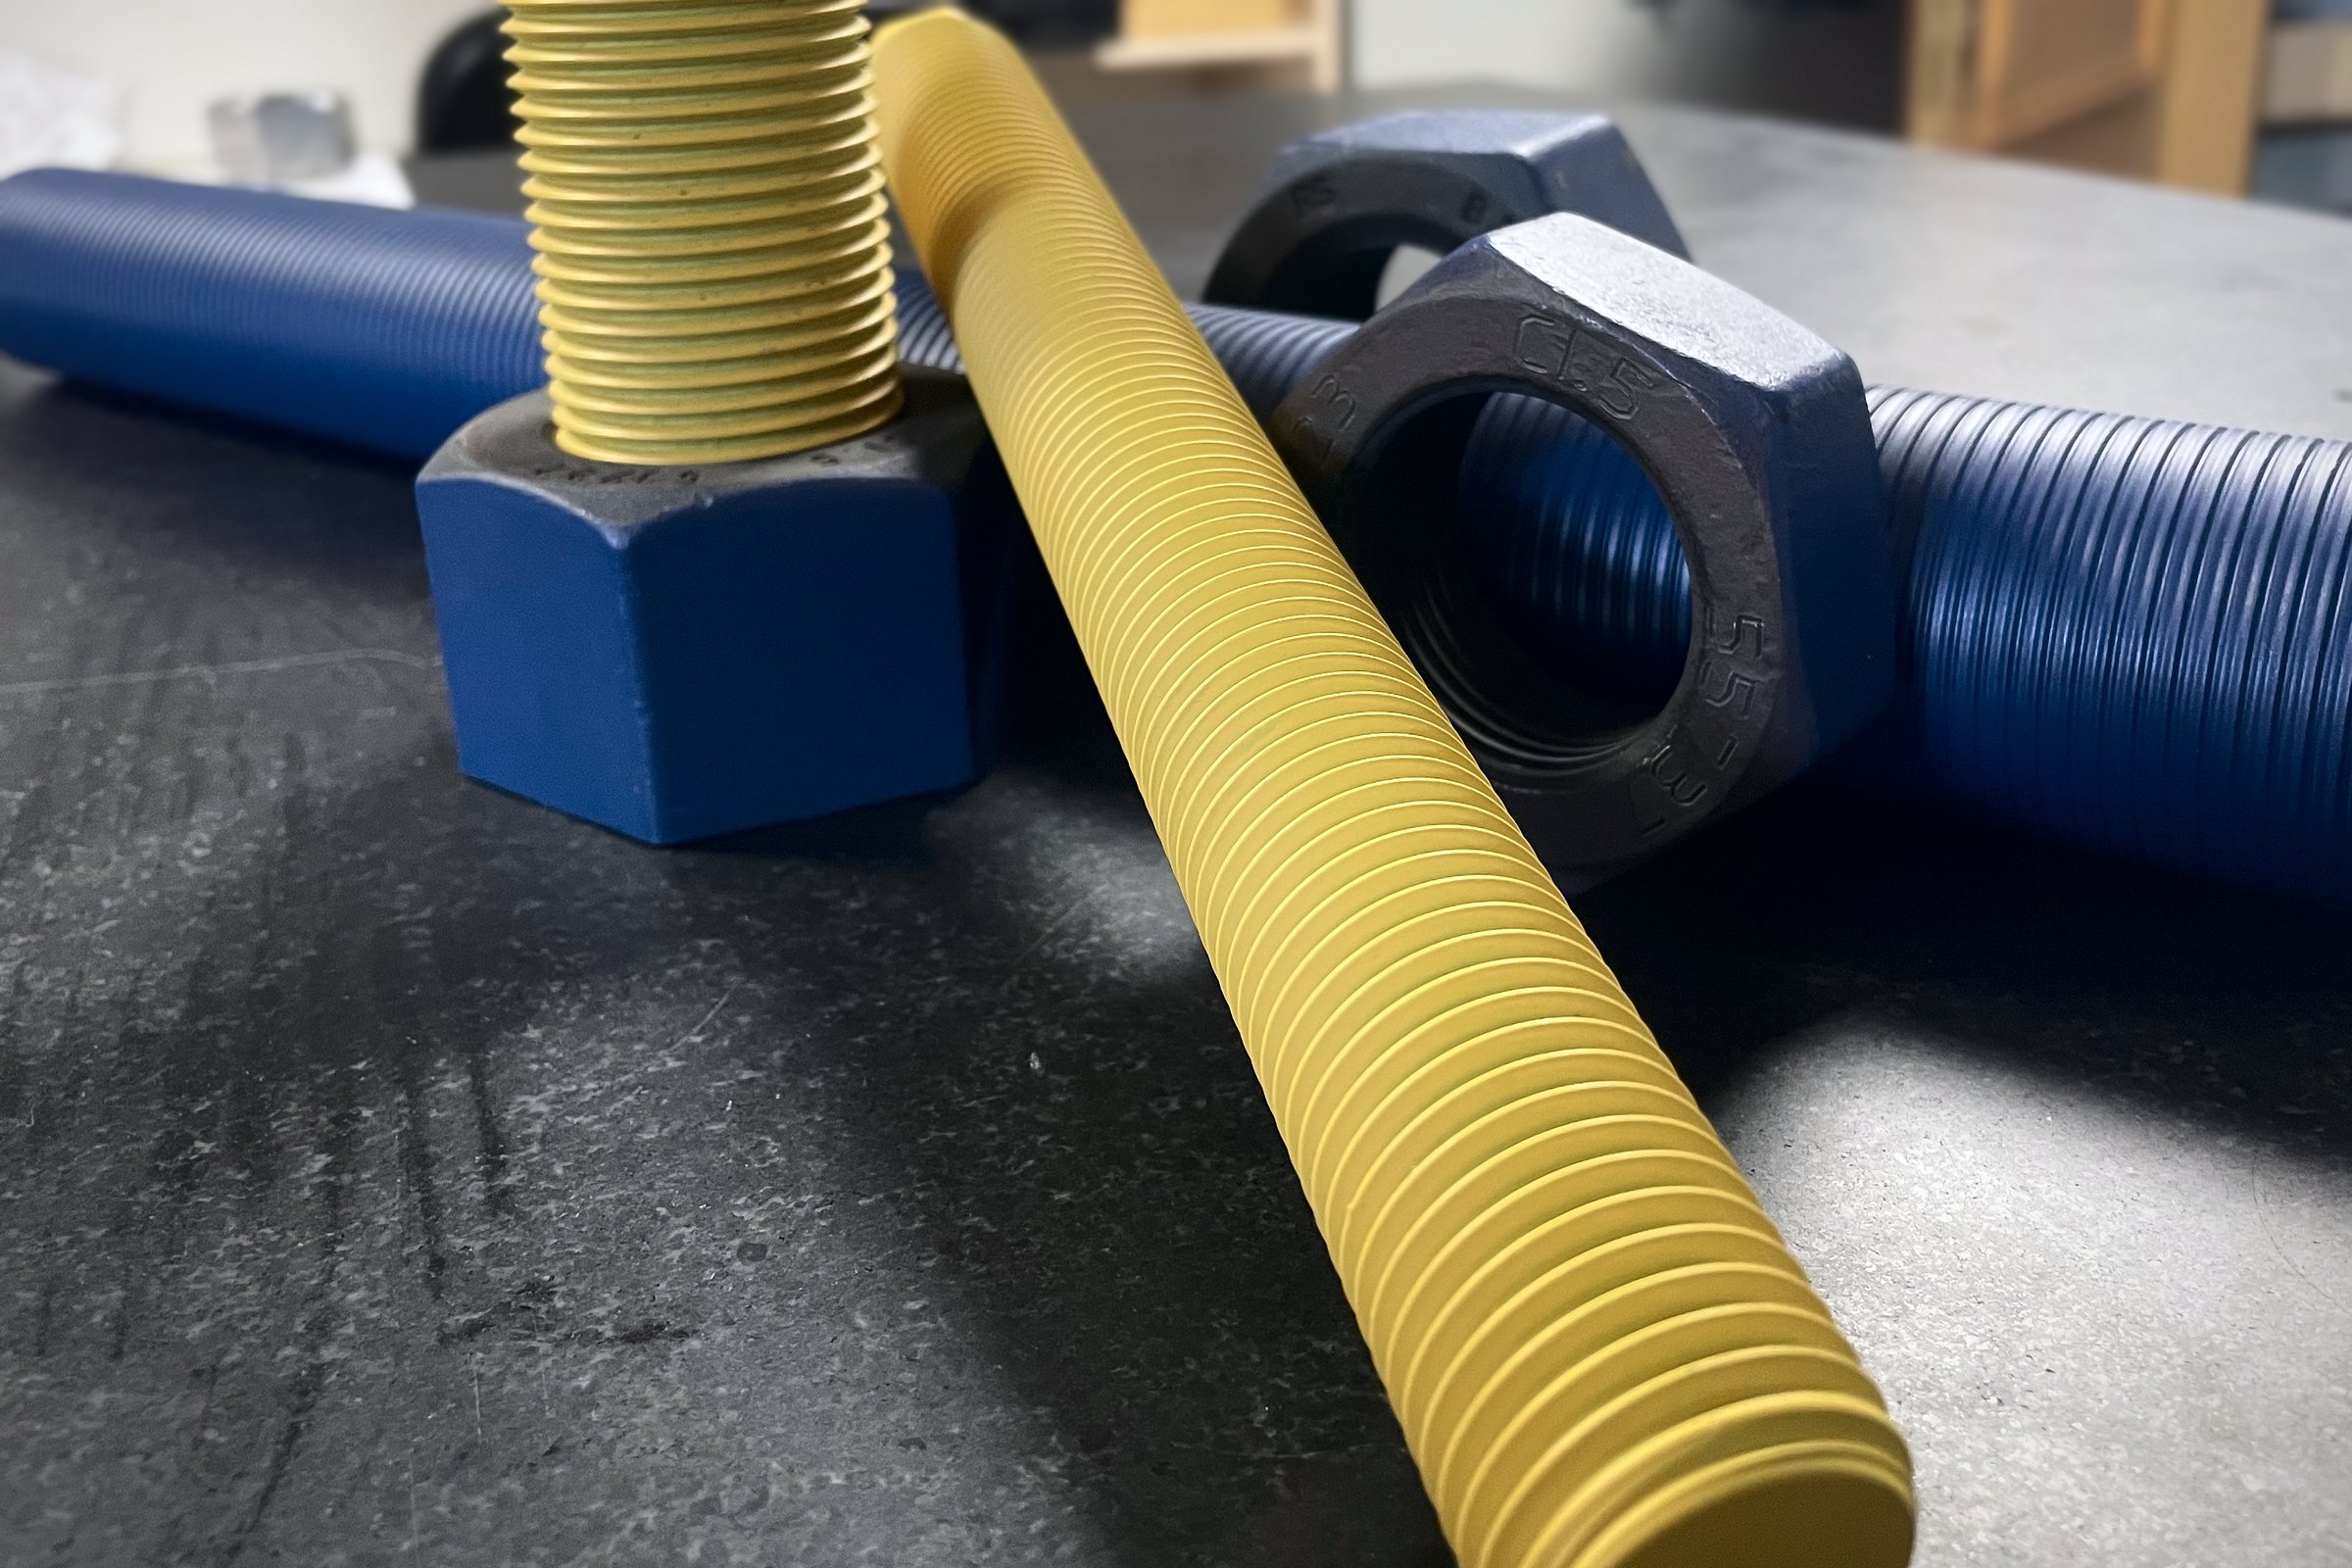
In zinc electroplating, the bolt is connected as the cathode in an electrolyte bath; zinc is deposited evenly as a metallic layer, usually 5 to 12 µm thick. A subsequent passivation, formerly chromating, increases protection and determines the colour: transparent blue, iridescent yellow or black. ISO 4042 governs the coating of fasteners; a code such as Zn5/Cn means 5 µm of zinc with thick-film passivation free of hexavalent chromium. Zinc protects steel cathodically: it sacrifices itself at scratches and edges before the steel rusts.
Where zinc electroplating is suitable
Bolts up to 8.8 in dry indoor areas or under cover, mechanical engineering, plants without chlorides, wherever appearance, low coating thickness and threads that stay within gauge matter. Zinc-nickel coatings achieve significantly better corrosion protection at the same thickness and are chosen when zinc flake is not an option.
Why approval is required for 10.9 and above
Pickling and zinc plating charge the steel with hydrogen. At strengths of about 1,000 N/mm² and above, i.e. 10.9 and 12.9, and for hardened parts from about 320 HV, this can lead to hydrogen embrittlement and delayed brittle fracture. Baking after coating reduces the risk but does not eliminate it; ISO 4042 and ISO 15330 describe this. RS Randack therefore applies electroplated zinc coatings to such parts only at the purchaser’s express request and risk, and usually proposes zinc flake or manganese phosphate with an anti-friction coating.
How RS Randack goes about it
Coating at partner companies working to ISO 9001, with baking as part of the process, checks before dispatch and on return, testing of coating thickness and thread gauging, and a coating certificate with the inspection certificate on request. Nuts are given a matching coating or an oversize thread so that the bolt and nut assembly still runs freely.
What you should specify
ISO 4042 code with coating thickness and passivation, colour, property class, for 10.9 and above the approval or a request for an alternative, and whether the nuts are to be coated as well.
Enquire about coated bolts with certificate
Urgent? You will hear from us within a few hours.